Structured PLC programming interview tracks: Q&A rounds, live-coding exercises graded by automated tests, and certificates (Pro) you can share with employers. Practice the problems that come up in real interviews.
Practice the explanation, the code and the diagnosis
Good candidates do more than recite definitions. They can explain a rung, build it correctly, trace a failed sequence and show the evidence that supports their conclusion.
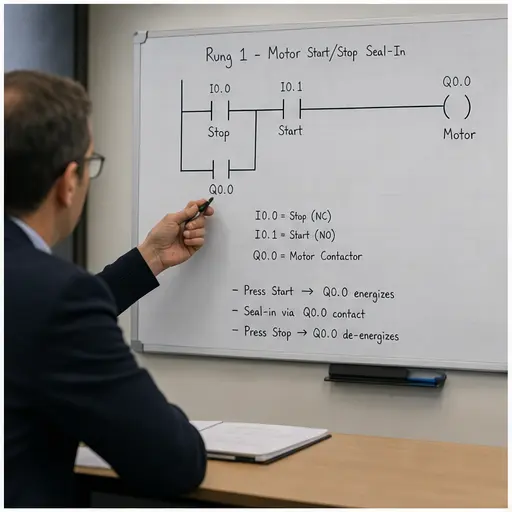
01Explain the requirement, current path, fail-safe stop and latch behavior in plain language.
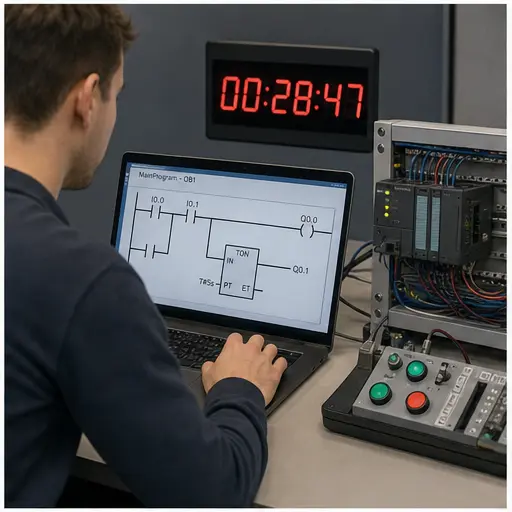
02Build and test a working rung against a live scenario instead of only memorizing model answers.
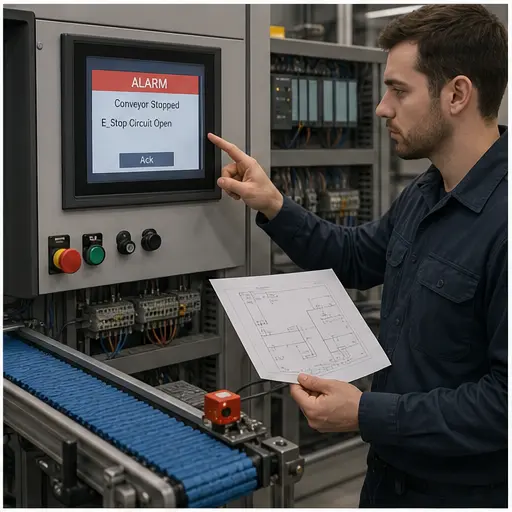
03Show a systematic signal-path diagnosis from symptom to raw input and physical evidence.
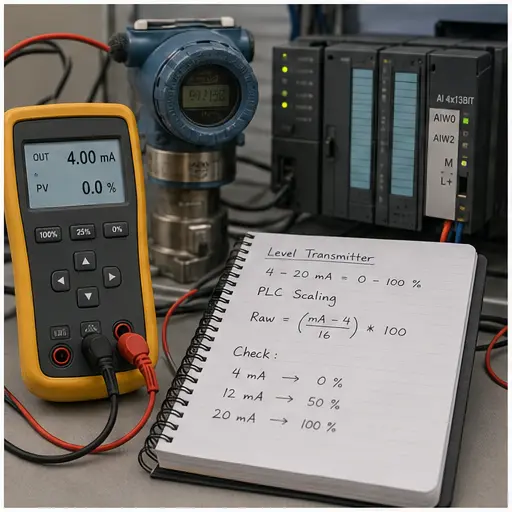
04Demonstrate that you can connect field measurement, raw counts and engineering units.
05Senior rounds probe design boundaries, failure response and the evidence behind a safe recovery.
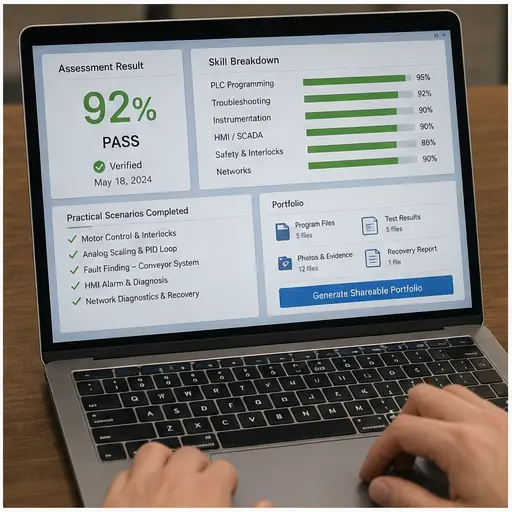
06Leave with concrete results and practical work that can support an employment conversation.
No PLC experience yet?
How to get a PLC job with no experience: what employers test
Most entry-level PLC and maintenance interviews check three skills. You can practice all three before anyone hires you.
1. Reading ladder logic
You get a printed rung and explain it: why the motor runs, what the stop button does, when the timer finishes. Practice with the PLC practice test.
2. Finding a fault
A machine has stopped. Interviewers want a method: symptom, input, rung, output, field device. Practice in the PLC troubleshooting simulator.
3. A practical task
Write a seal-in, an interlock or a timer sequence, on paper or in a simulator. The live-coding rounds below grade this the same way.
How to prove it without a PLC job on your resume
Graded practice: a scenario only passes when the simulated machine behaves correctly, so a pass means your logic works.
Portfolio projects: solve machine scenarios such as a motor starter, conveyor sort or traffic light, and export a portfolio PDF (Pro) to bring to the interview.
A verifiable certificate: passing a certificate-eligible track with Pro gives you a certificate with a public verification link. The Junior track is free but has no certificate. It is not a vendor or industry credential; see the PLC technician certificate guide for those.
Write a working program from a brief against a live scenario. Automated tests grade it, so you know whether it actually works — exactly what employers test.
Q&A rounds with graded answers
Interview-style questions on fundamentals, analog I/O, PID, safety, and communication protocols. Your answers are scored against model answers with explanations.
Verifiable certificates
Pass a certificate-eligible track and earn a certificate with a unique verification URL (issuing it needs Pro; the free Junior track has none). Share it in your portfolio or LinkedIn profile.
Interview tracks
6 interview tracks by role and seniority
Junior
Junior Controls Engineer
Ladder fundamentals, seal-in rungs, basic timers, motor control. Suitable for entry-level applicants.
Select the track that matches the role you are applying for: junior, mid, senior, or specialist.
02
Complete Q&A round
Answer interview-style questions on PLC fundamentals. Graded against model answers.
03
Complete coding round
Write a working PLC program against a live scenario. The auto-grader evaluates it against the test suite.
04
Earn your certificate
Pass a certificate-eligible track and, with Pro, download your verifiable certificate. Share the verification link with employers.
Common questions
Common PLC interview questions — with model answers
These are the fundamentals that come up in almost every PLC programming interview, from junior controls roles to senior process automation. Read the model answer, then practise the same concept live in a graded scenario — passive reading does not survive the pressure of a live technical round.
The scan cycle: read inputs → execute program → update outputs → repeat. The single most-asked PLC interview question.The seal-in rung — interviewers ask you to draw three-wire motor control on a whiteboard from memory.
Q1. Walk me through the PLC scan cycle.
A PLC repeats a fixed cycle: (1) read all physical inputs into the input image table, (2) execute the user program rung-by-rung top-to-bottom, left-to-right, writing results to the output image table, (3) update the physical outputs from that table, then housekeeping/comms — and repeat. Outputs do not change mid-scan, which is why scan order matters and why a coil written low later in the program overrides an earlier rung.
Q2. Why must a Stop button be wired to a normally-closed contact?
For fail-safe operation. A normally-closed (NC) Stop is examined with an XIO instruction so the rung is true when the button is not pressed. If the wire breaks or a terminal comes loose, the circuit sees an open — the same as a press — and the machine stops. A normally-open Stop would fail dangerously: a broken wire would leave the machine running with no way to stop it.
Q3. What is a seal-in (latch) rung and where is it used?
A seal-in is a parallel holding contact of the output placed around the momentary Start contact. Once Start energises the coil, the output’s own contact keeps the rung true after Start is released; an NC Stop in series breaks it. It is the basis of three-wire motor control and appears in nearly every real control program.
Q4. Explain the difference between TON, TOF, and RTO timers.
A TON (on-delay) starts timing when its rung goes true and sets its Done bit when accumulated time reaches the preset; if the rung goes false the accumulator resets to zero. A TOF (off-delay) keeps its output on for the preset after the rung goes false. An RTO (retentive) holds its accumulated value when the rung goes false and needs a separate RES instruction to reset — used where elapsed time must survive power or logic interruptions.
Q5. How would you troubleshoot a machine that suddenly stopped?
Work systematically rather than randomly: check the PLC and fault indicators, look at the program status (which rung is not making true), then divide and conquer — confirm the input the rung needs is present (force/monitor it), trace back to the field device with a meter (24 VDC present? sensor switching? wiring intact?). Isolate to the smallest failing element before changing anything, then verify the fix.
Q6. What is the difference between a normally-open and normally-closed contact in ladder logic?
A normally-open contact (XIC, "examine if closed") passes power when its referenced bit is 1/true. A normally-closed contact (XIO, "examine if open") passes power when its bit is 0/false. The contact symbol describes how it behaves in the program, which is independent of whether the physical field device is wired NO or NC — a common source of confusion that interviewers probe.
Timers (TON / TOF / RTO) — a guaranteed interview topic. Know how each handles a rung going false.NO vs NC contacts (XIC / XIO) and the rest of the instruction set you will be asked to read and write on the spot.Discrete I/O, sinking vs sourcing — the wiring fundamentals technical screens cover before any coding round.
The five IEC 61131-3 languages — senior interviews ask which language suits which job and why ladder dominates discrete control.
Most PLC interviews have a technical screen (verbal Q&A on fundamentals: scan cycle, timers, safety, PID) and a practical exercise (write a program to solve a machine control problem — sometimes on paper, sometimes live in an IDE or simulator). Our interview tracks are structured around both components.
Each track has multiple rounds: a Q&A round (questions matching the seniority level), a live-coding round (write a working program against a live scenario), and a review. Tracks range from junior (1–2 years experience) to senior (5+ years, including safety and PID).
Most of them do. Passing a certificate-eligible track earns a downloadable certificate with a unique verification code, dated and showing the track name and score. Issuing a new certificate needs a Pro plan, and the free Junior track does not award one. A certificate you have already earned stays downloadable.
Scan cycle and execution order, seal-in rungs and latch circuits, timer and counter programming, analog scaling, PID control, safety interlocks and E-stop circuits, Modbus communication basics, and troubleshooting methodology.
Reading questions passively does not prepare you to write code under pressure. The live-coding rounds make you produce working programs against a scenario, the way a real technical interview does. Objective grading means you know whether your program actually works, not just whether it looks plausible.
Yes. The certificate includes a verification URL. While it is not a vendor certification, it demonstrates hands-on programming ability in a verifiable format — more credible than listing "PLC programming" on a resume without supporting evidence.
The fundamentals come up almost every time: explain the PLC scan cycle (read inputs, execute program, update outputs, repeat); why a Stop button must be normally-closed for fail-safe operation; what a seal-in/latch rung is and where it is used; the difference between TON, TOF, and RTO timers; the difference between a normally-open (XIC) and normally-closed (XIO) contact; and how you troubleshoot a machine that suddenly stopped. We work through each of these with model answers on this page and let you practice the same concepts in graded scenarios.
Live-coding rounds ask you to write a working program from a short brief — typically motor start/stop with a seal-in, a timed sequence, or a counter-based batch. The only reliable preparation is to write and run programs against test cases, not to read solutions. Our coding tracks give you a brief, a scenario to run against and an auto-grader that tells you whether your program actually works. Rounds show a target duration, but results come from the automated tests, not the clock.
Ace your PLC programming interview
Graded tracks, live coding, verifiable certificates (Pro). Start free.