TL;DR: Thermocouples (TC) are rugged, cover -200 °C to +1260 °C, and use standard copper extension wire — but are only ±1.5–2.5 °C accurate. RTDs (PT100) are more accurate (±0.15–0.5 °C), more stable over time, and more linear — but cost more and require matched 3-wire or 4-wire connection. Thermistors are cheap and accurate over a narrow range (0–100 °C) but not standard in industrial PLC systems. For most industrial PLC applications: thermocouple for high-temperature or high-density measurement, RTD for precision process control.
Temperature measurement accounts for a significant fraction of all analog inputs in a typical industrial plant. Choosing the wrong sensor type introduces systematic error that no software calibration can fully correct. The three main technologies — thermocouple, RTD (Resistance Temperature Detector), and thermistor — each solve a different point in the accuracy/range/cost trade-off space.
Thermocouple: Wide Range, Simple, Rugged
A thermocouple is formed by joining two dissimilar metal wires. At the measurement junction (the sensing tip), the Seebeck effect produces a small voltage — typically 0–70 mV — proportional to the temperature difference between the hot junction (the tip) and the cold reference junction (where the wires connect to the module). The PLC module measures this voltage and converts it to temperature using a polynomial linearisation table.
Type K (chromel/alumel) is the industrial standard. Range: -200 °C to +1260 °C. Sensitivity: ≈41 µV/°C at mid-range. Accuracy: ±1.5 °C (Class 1) to ±2.5 °C (Class 2). The output curve is nonlinear, which the input module corrects automatically.
Other common types:
- Type J (iron/constantan): -40 °C to +750 °C, ≈52 µV/°C. Common in older North American equipment. Avoid in oxidising atmospheres above 500 °C.
- Type T (copper/constantan): -200 °C to +350 °C, ≈43 µV/°C. Best accuracy among base-metal types. Suitable for cryogenic applications.
- Type E (chromel/constantan): highest output (68 µV/°C) — good for detecting small temperature differences.
- Types R, S, B (platinum/rhodium): for furnace temperatures 600–1820 °C. Very low output (6–12 µV/°C); requires shielded cable and precise measurement.
Cold junction compensation (CJC) is critical. The module measures the ambient temperature at the terminal block (the cold junction) and adds the correction to the measured voltage. This is done automatically in every modern thermocouple input module. Using copper wire to extend a thermocouple — instead of proper extension wire matching the thermocouple type — introduces a spurious junction at the connection point and causes a systematic temperature error.
Wiring: thermocouple cables use the same metal pair as the sensor. Type K positive lead is yellow, negative is red (IEC 60584 colors). Cable is inherently 2-wire (the thermocouple itself is the measurement circuit). PLC modules: Siemens SM331 TC, Allen-Bradley 1756-IT6I, Schneider TM2AMI4LT.
RTD / PT100: Accurate, Stable, Linear
An RTD measures temperature via the increase in electrical resistance of a platinum element. PT100 — the IEC 60751 standard — has exactly 100 Ω at 0 °C. The relationship is nearly linear: resistance increases approximately 0.385 Ω per °C (the α = 0.00385 coefficient). At 100 °C the resistance is ≈138.5 Ω; at 400 °C it is ≈254 Ω.
Because resistance is measured rather than a tiny millivolt signal, PT100 offers significantly better accuracy and noise immunity. Accuracy classes under IEC 60751:
- Class AA: ±(0.10 + 0.0017|T|) °C — used in laboratory and pharmaceutical applications
- Class A: ±(0.15 + 0.002|T|) °C — precision industrial measurement
- Class B: ±(0.30 + 0.005|T|) °C — standard industrial PT100
2-wire, 3-wire, and 4-wire connections exist because the resistance of the copper cable adds to the platinum element resistance and creates a temperature error:
- 2-wire: cable resistance included in reading. ±0.5 Ω per metre of cable = ±1.3 °C per metre of round-trip lead. Only acceptable for cable runs under 1 m.
- 3-wire (most common): a third conductor allows the module to measure and subtract cable resistance. Accurate to ±0.1 °C when all three conductors are the same gauge and length.
- 4-wire (Kelvin): two current-carrying wires, two voltage-sensing wires. Lead resistance has zero effect. Used in GMP pharmaceutical and metrological applications.
Stability is PT100's strongest argument: a well-installed PT100 drifts less than 0.05 °C/year. A Type K thermocouple in continuous service at 500 °C+ can drift 5–10 °C per year due to physical changes in the wire metals.
Wiring: the PLC module supplies a precise excitation current (typically 1–2 mA) through the PT100 element and measures the resulting voltage. Modules: Siemens SM331 RTD, Allen-Bradley 1756-IR6I, Schneider TM2AMI4LT (same module handles both TC and RTD types via parameter settings on many platforms).
Thermistor: Narrow Range, High Sensitivity, Low Cost
A thermistor is a semiconductor resistor whose resistance changes sharply with temperature. NTC (Negative Temperature Coefficient) thermistors decrease in resistance as temperature rises — a 10 kΩ NTC thermistor at 25 °C might drop to 3.5 kΩ at 50 °C. This large resistance change produces very high sensitivity over a narrow range.
Advantages: extremely sensitive, low cost, compact, fast response. Disadvantages: highly nonlinear (requires a Steinhart-Hart equation correction), limited range (typically 0–150 °C for industrial types), not standardized (each manufacturer has a different resistance-temperature curve).
Thermistors are not standard in industrial PLC systems. You will not find dedicated thermistor input modules in Allen-Bradley, Siemens, or Schneider catalogs. Thermistors appear in HVAC equipment (fan motors, compressor windings), battery management systems, and consumer electronics — not typically in PLC-controlled processes. If you encounter a thermistor in an industrial panel it is usually an equipment-protection device (motor winding thermal cutout) wired to a relay or trip unit, not a PLC analog input.
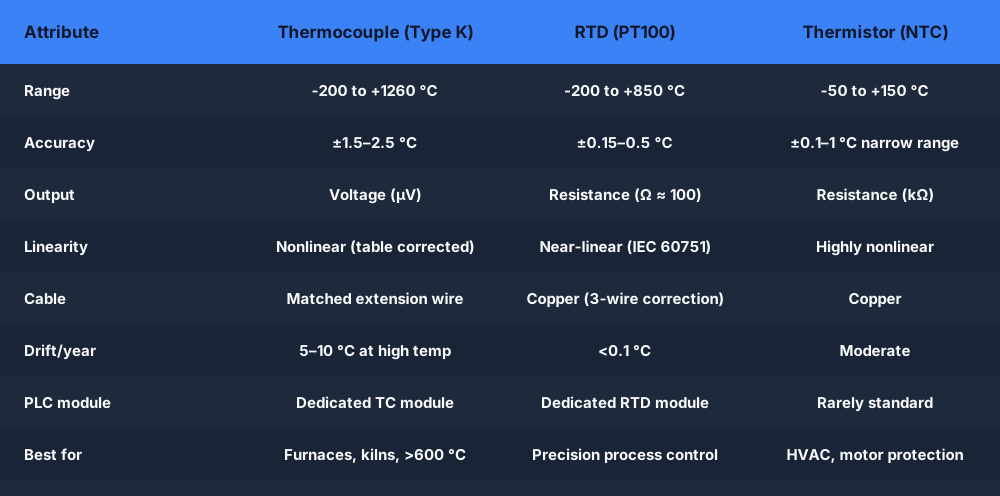
Side-by-Side Comparison
| Thermocouple (Type K) | RTD (PT100) | Thermistor (NTC) | |
|---|---|---|---|
| Temperature range | -200 °C to +1260 °C | -200 °C to +850 °C | -50 °C to +150 °C (typical) |
| Accuracy | ±1.5–2.5 °C | ±0.15–0.5 °C | ±0.1–1 °C (narrow range) |
| Output | Voltage (µV) | Resistance (Ω) | Resistance (kΩ) |
| Linearity | Nonlinear (table corrected) | Near-linear (IEC 60751) | Highly nonlinear |
| Cable | Matched extension wire (expensive) | Any copper (3-wire correction) | Any copper |
| Stability / drift | 5–10 °C/year at high temp | <0.1 °C/year | Moderate |
| PLC support | Standard dedicated TC module | Standard dedicated RTD module | Rarely supported directly |
| Relative cost | Low sensor, moderate module | Moderate sensor and module | Very low |
| Best application | Furnaces, kilns, exhaust >600 °C | Process control, food, pharma | HVAC, motor protection |
Which One Should You Choose?
Choose a thermocouple when:
- Process temperature exceeds 600 °C — RTDs do not survive
- High-density measurement (10+ points per panel) — lower cost per channel
- Existing installation uses thermocouple infrastructure (extension cable trays already in place)
- The accuracy budget allows ±2 °C — which covers most industrial processes
Choose an RTD (PT100) when:
- Required accuracy is better than ±1 °C (food processing, pharmaceutical batch)
- Long-term stability matters — pharmaceutical validation requires drift to be documented over years
- Temperature differences of 1–5 °C are significant (heat exchanger efficiency, fermentation delta T)
- Process temperature is below 600 °C — the entire industrial sweet spot
Avoid thermistors for new PLC designs unless you are integrating motor protection relays that already have a thermistor circuit, or replicating an existing HVAC system that uses them.
PLC Module Wiring Gotchas
Thermocouple: Never extend a thermocouple cable with copper wire. The copper junction introduces a thermocouple effect at the connection point — a 20 °C ambient swing in the junction box causes a 0.8–1 °C reading error. Always use extension grade thermocouple wire of the matching type.
PT100 3-wire: All three wires must be the same gauge and the same length for the module's lead-resistance compensation to work. If you cut one lead shorter than the others, you introduce an uncompensated resistance error. Some installers accidentally run only two wires and short the third at the head — this reverts to 2-wire accuracy.
PT100 4-wire: Ensure the module supports 4-wire mode (not all channels do). The two current leads (I+, I-) and two voltage sensing leads (V+, V-) must be correctly connected per the module wiring diagram — swapping any pair defeats the Kelvin compensation.
Frequently Asked Questions
Q: Is a thermocouple better than an RTD?
A: Neither is universally better. A thermocouple covers a wider range (up to 1260 °C vs 850 °C for PT100) and is lower cost for high-density installations. An RTD is more accurate (±0.15–0.5 °C vs ±1.5–2.5 °C), more stable, and more linear. For most precision process control applications below 600 °C, an RTD is the better choice. For furnaces, kilns, or high-temperature exhaust monitoring, a thermocouple is the only practical option.
Q: Can I use a PT100 with a thermocouple input module?
A: No. A thermocouple input module expects a microvolt-level voltage signal with cold junction compensation. A PT100 outputs a resistance change around 100–400 Ω. They are fundamentally different signal types requiring different input modules. Using a PT100 on a thermocouple module will give garbage readings.
Q: What is the difference between PT100 and PT1000?
A: Both are platinum resistance thermometers with the same IEC 60751 temperature coefficient (α = 0.00385). PT100 has a base resistance of 100 Ω at 0 °C; PT1000 has a base resistance of 1000 Ω at 0 °C. PT1000 is used where lead resistance is significant (long cable runs) — the ratio of lead resistance to element resistance is ten times smaller. Most industrial PLC RTD modules support both; check the module datasheet.
Q: Why does my thermocouple read 20–30 °C too high even at ambient temperature?
A: The most common cause is missing or incorrect cold junction compensation. The module's CJC sensor is measuring the wrong temperature — check that the module is within its ambient temperature specification and that the terminal block is not exposed to direct heat sources. A second cause is extension wire polarity reversal — if the + and − leads are swapped, the output doubles the CJC error.
The interactive thermocouple sensor page shows the mV output rising with temperature and the cold junction compensation in action. The RTD / PT100 page shows the resistance climb and the 3-wire compensation principle.
Practice wiring both sensor types into a PLC temperature control loop with the fermentation temperature control scenario.