Start with the controller, trace field I/O into trustworthy tags, then connect HMI screens, Modbus data, alarms and process behaviour. Begin with a guided browser program before choosing a plan.
No account for the first program. Free accounts do not require a card or expire.
Real PLC SCADA training footage
See this exact skill in the working simulator.
Watch the real browser product respond to the task on this page, then try the same practical workflow yourself. No slides, concept mockups, install, or credit card.
HMI Simulator Online — Build an Operator Screen on a Live PLC
From field signal to operator decision
Learn PLC and SCADA as one traceable control system.
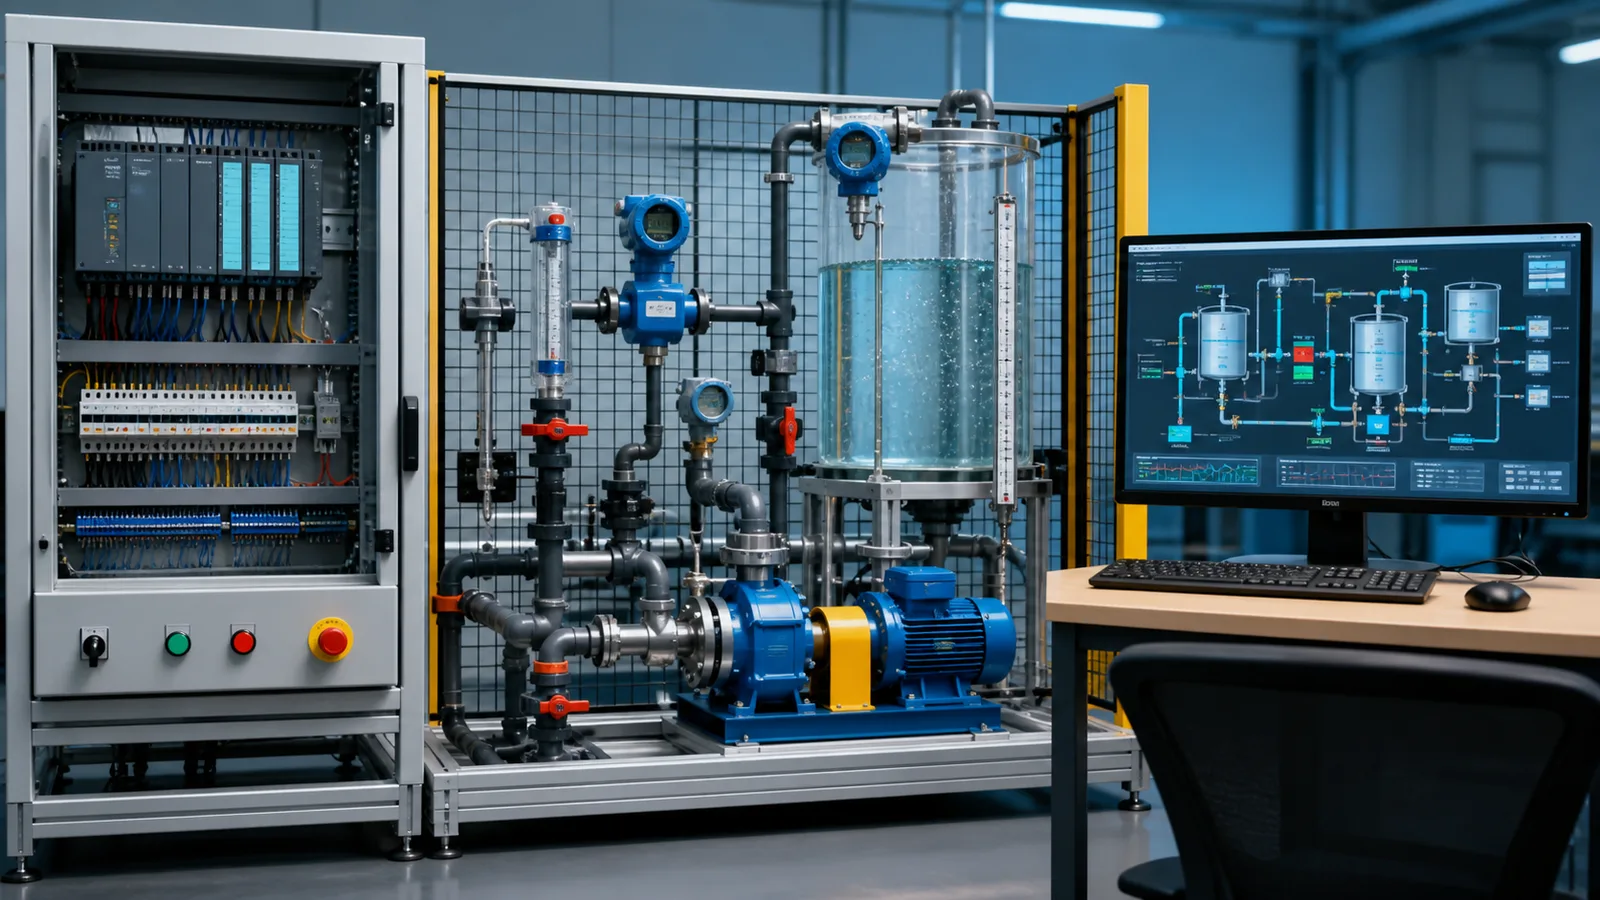
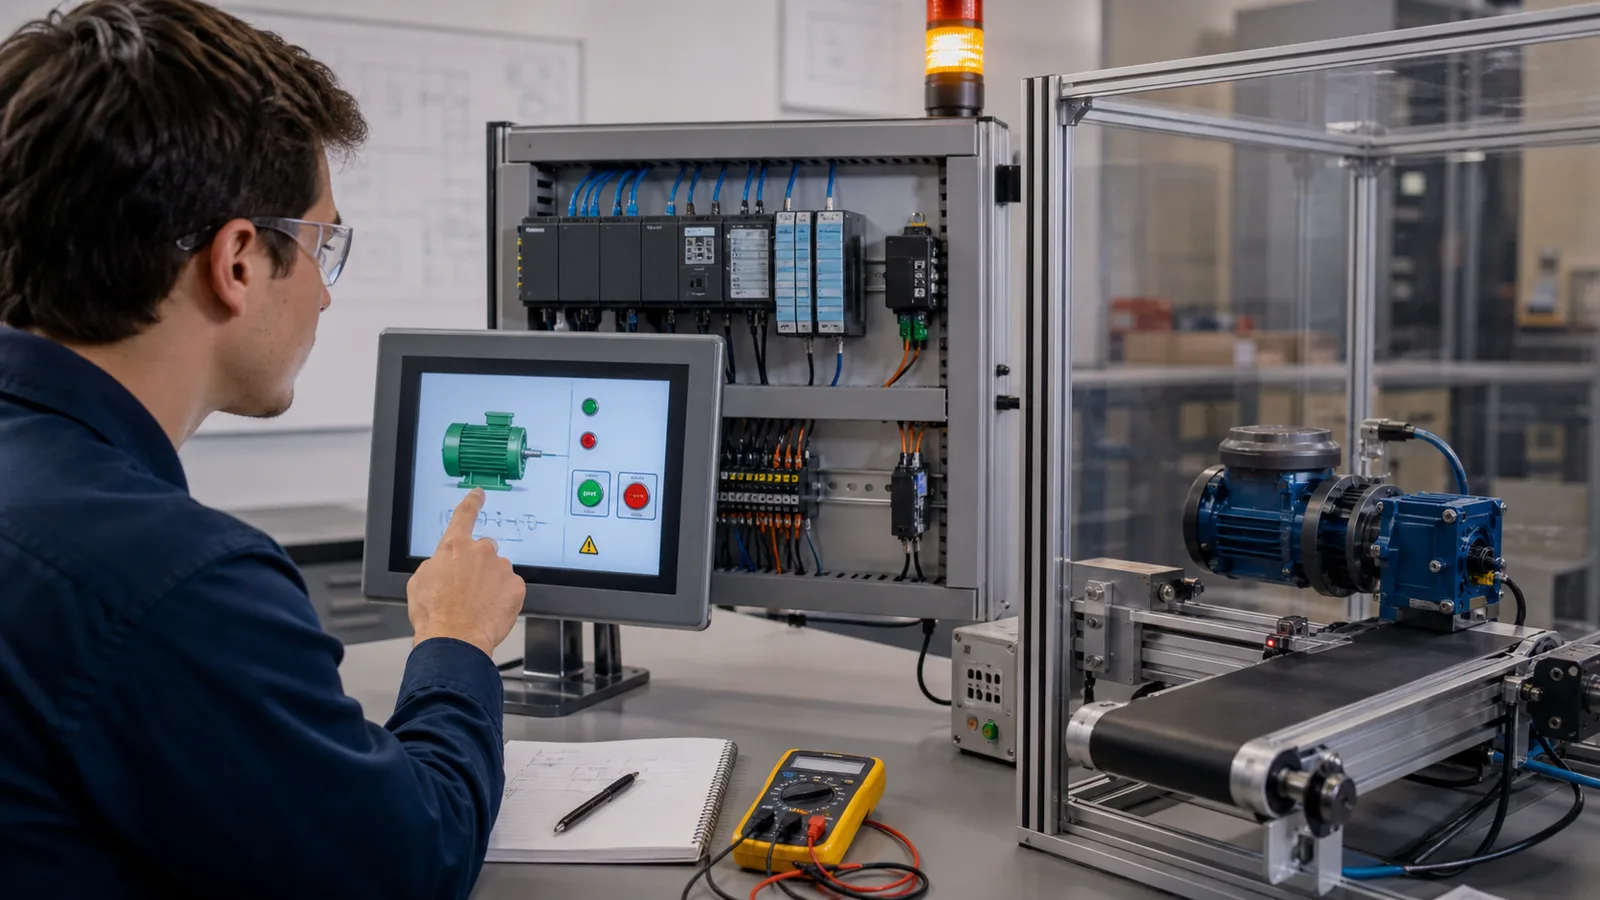
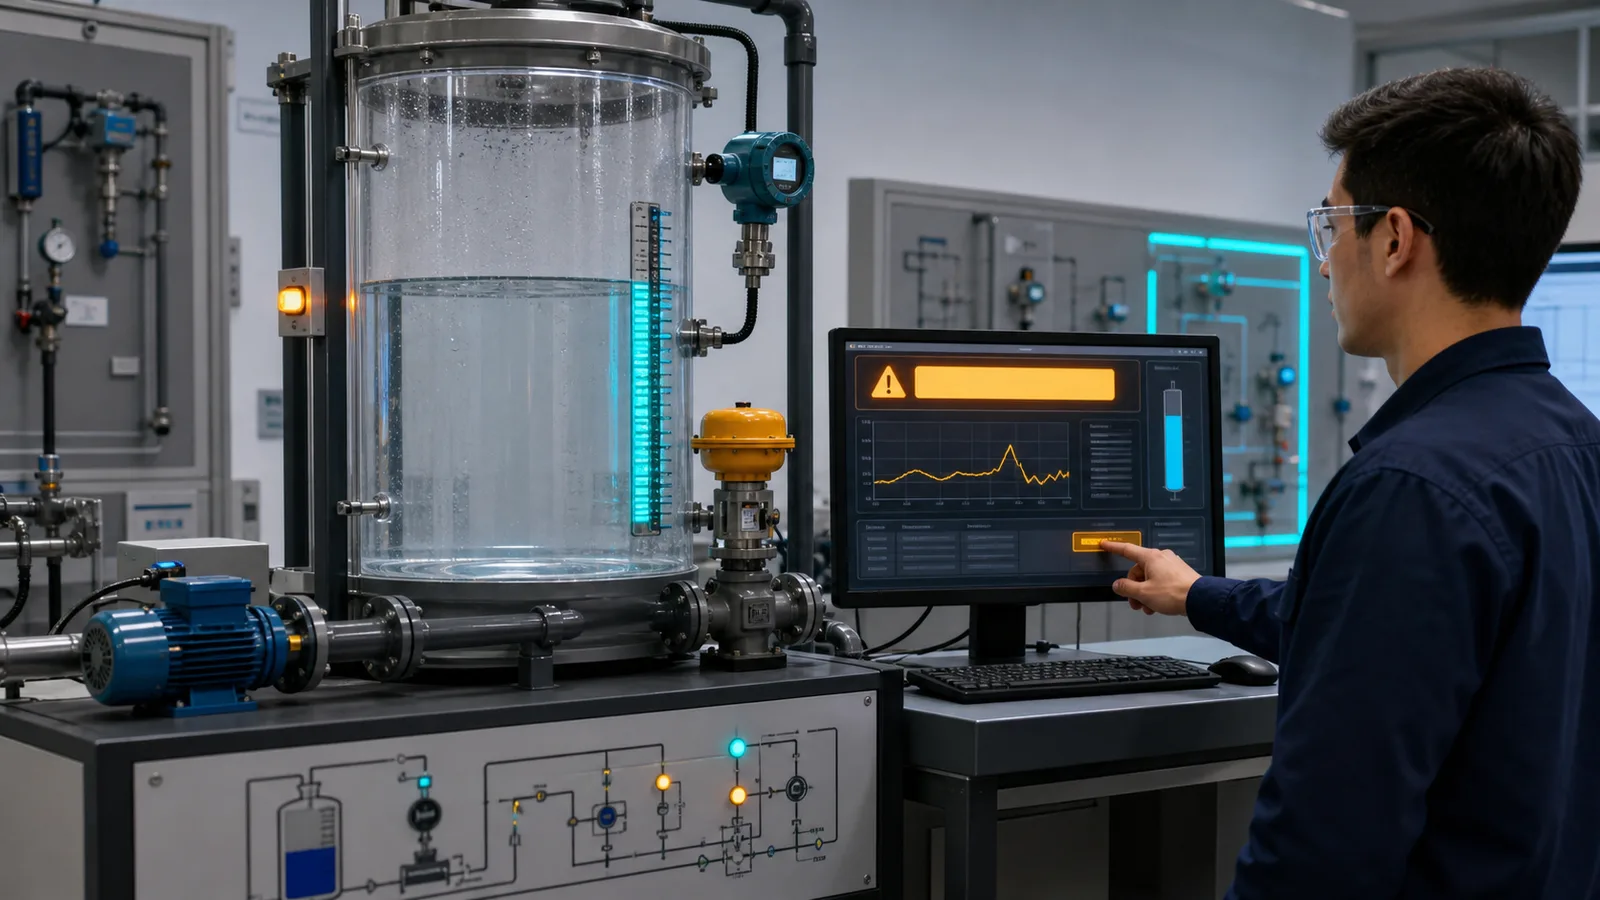
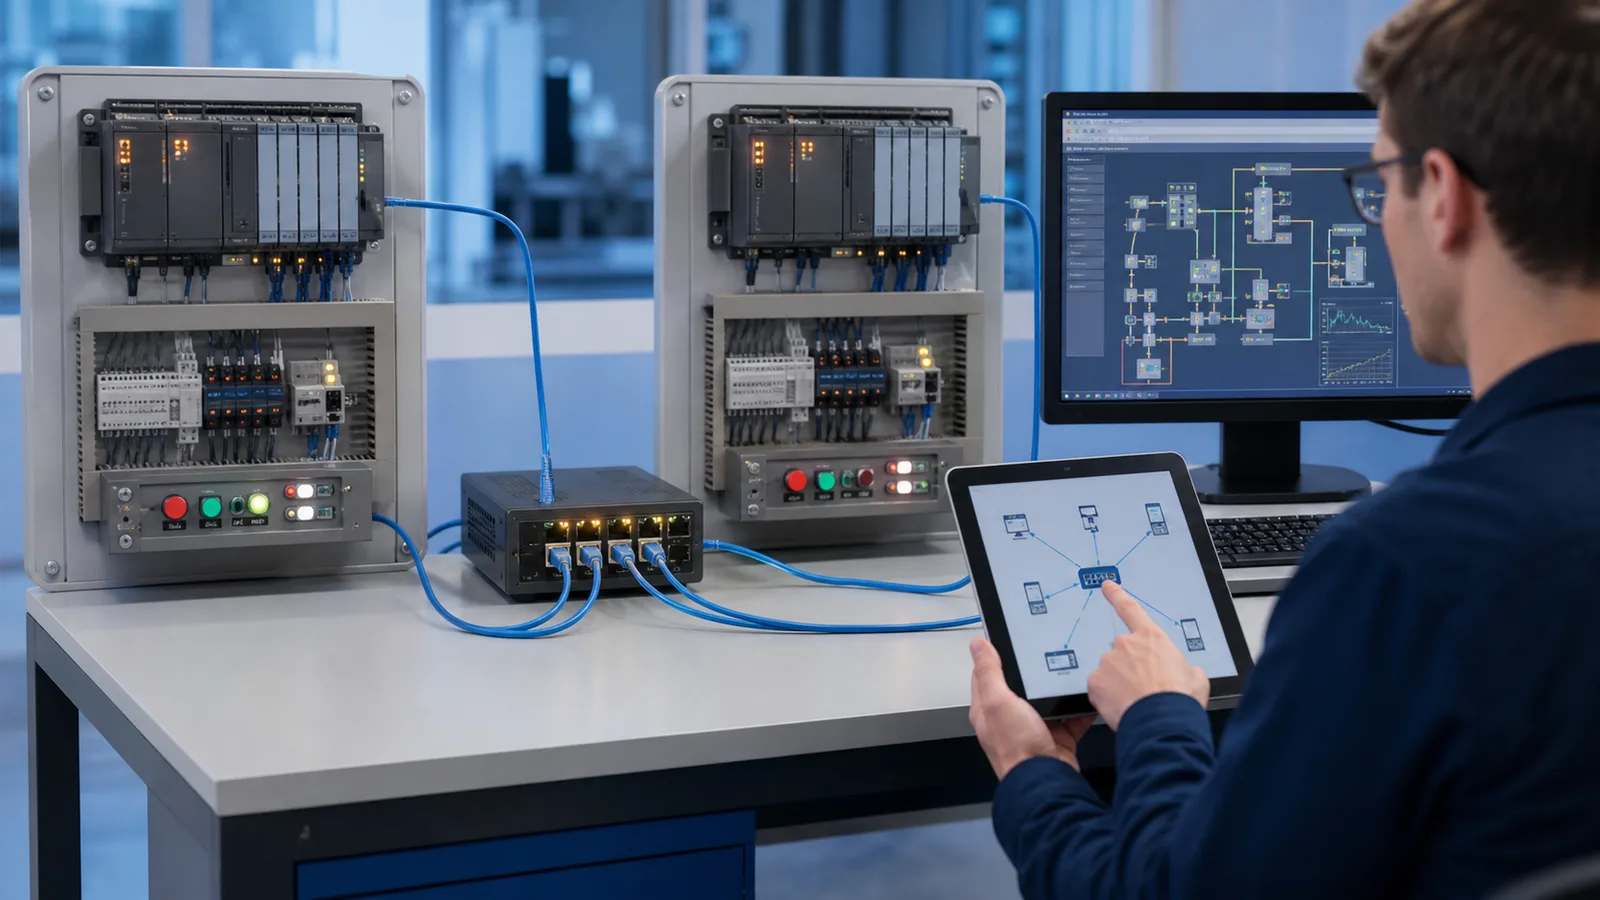
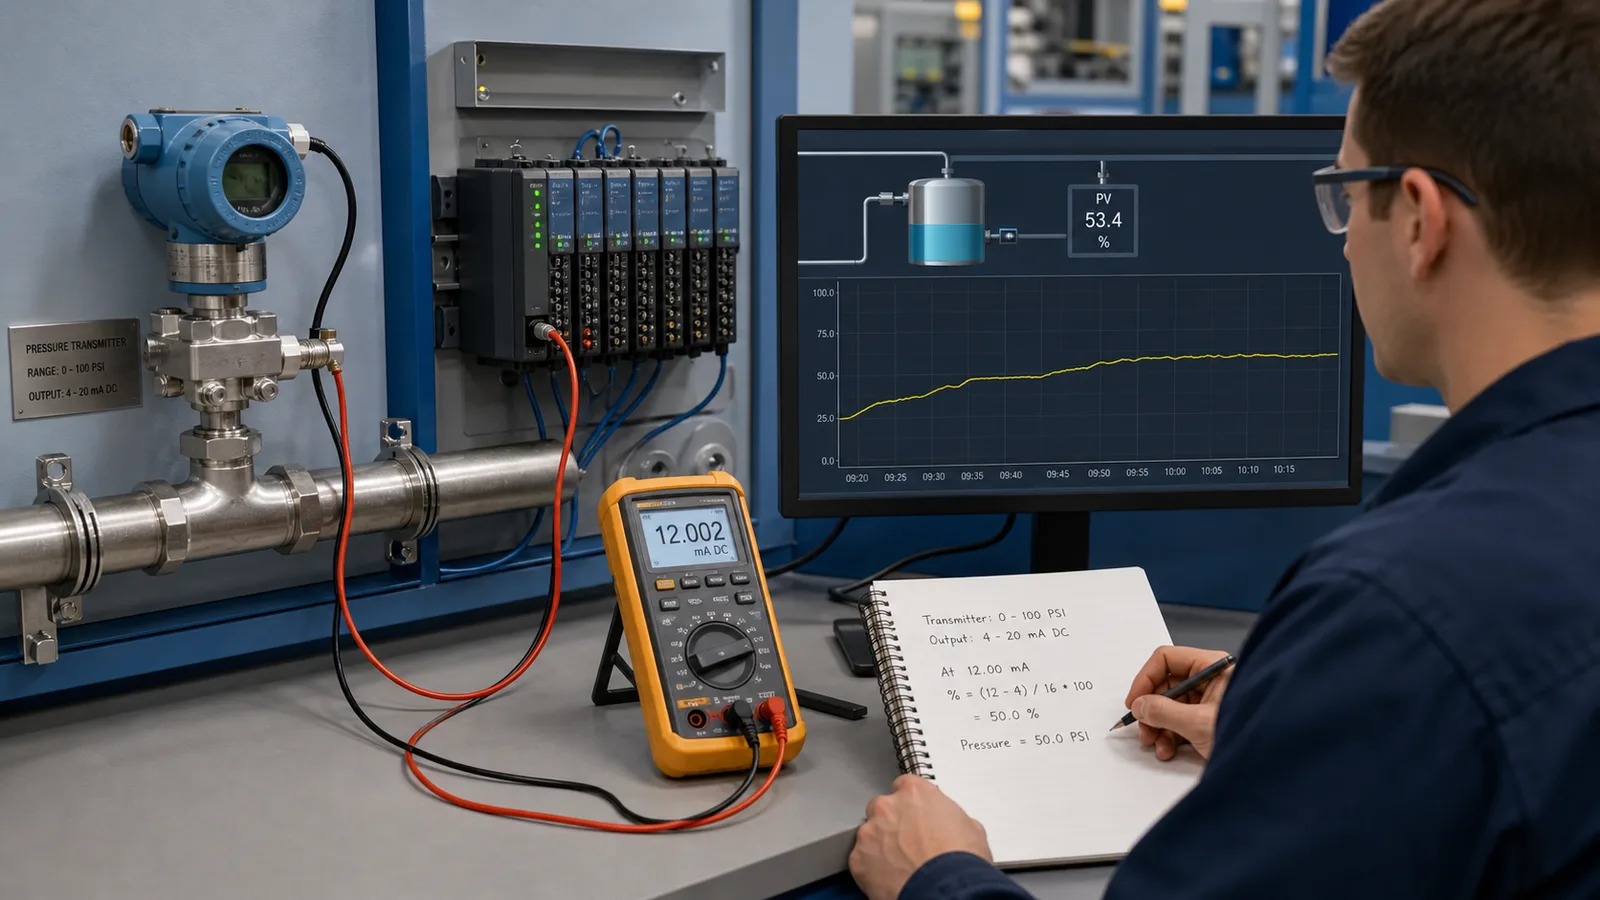
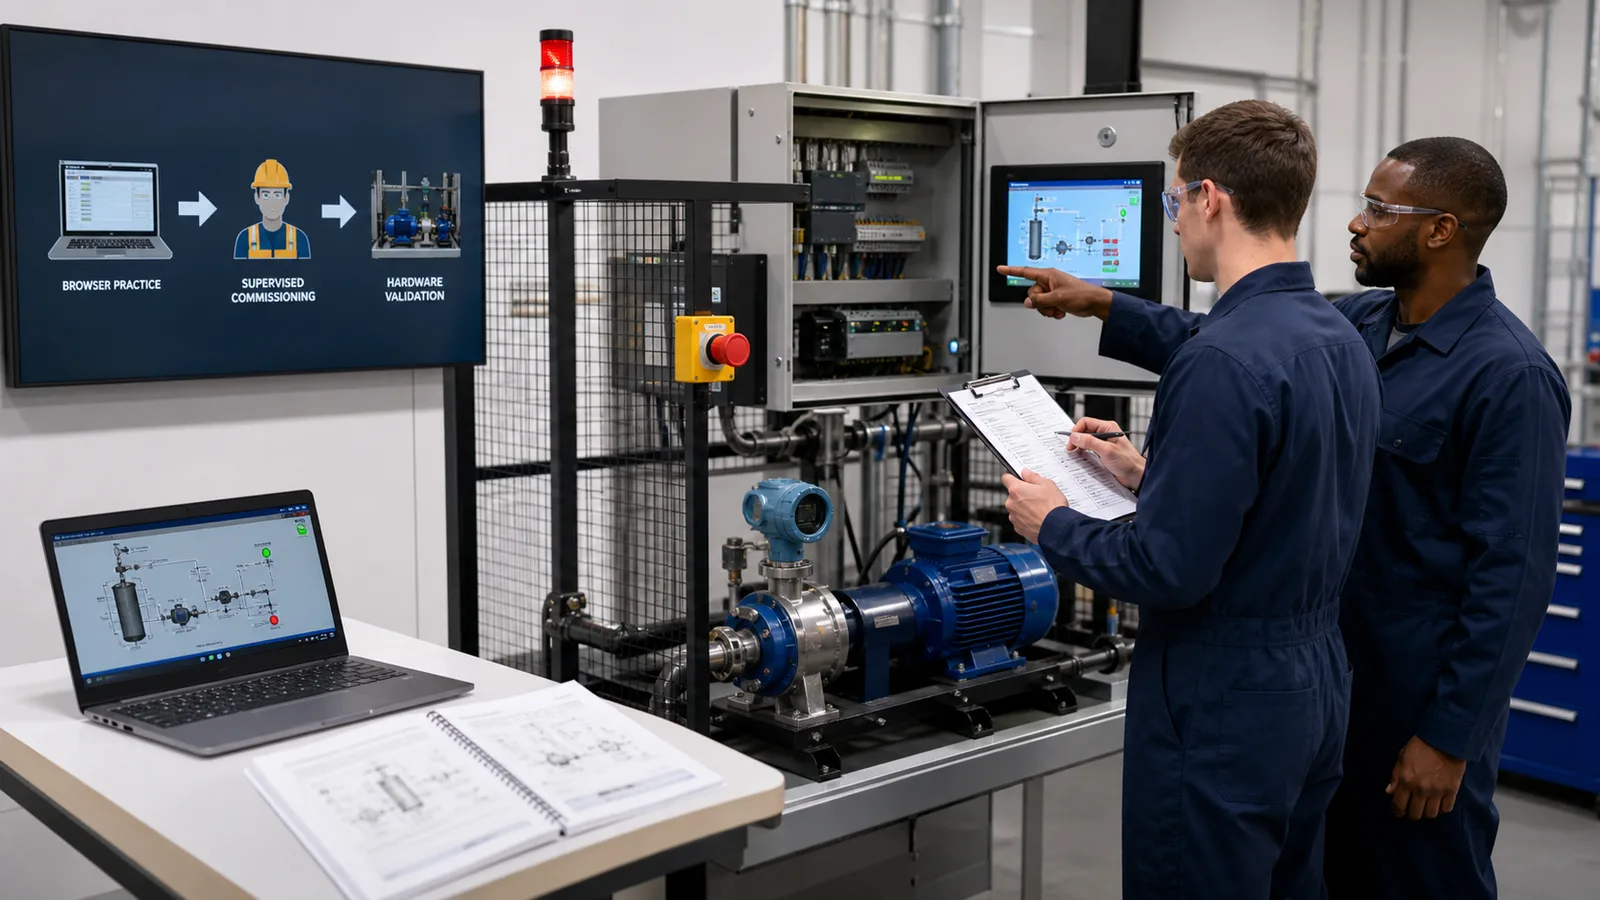
These six scenes make the data path concrete: instrument, I/O, control logic, industrial network, HMI response and supervised commissioning. Every screen value should have a physical source and a testable purpose.
01Read the stack from left to right: field signals enter the controller, control logic changes machine state, and the supervisory screen presents trustworthy tags.
02An HMI control only becomes useful when its command, permissive, feedback and fault states are mapped to meaningful controller tags.
03Alarm training joins the banner to the physical cause: verify the process, investigate evidence, correct the condition and confirm recovery.
04A tag path crosses devices and links. Learn where to test when the HMI value is bad: field, I/O, PLC, network, driver or display.
05Analog values must keep their units and range through the whole chain—from loop current and raw counts to scaled tag and trend.
06Simulation builds the reasoning; supervised hardware work adds electrical safety, measurement, controller configuration and commissioning evidence.
The discipline
What PLC SCADA programming actually is
A PLC (Programmable Logic Controller) is the controller that makes machines move. A SCADA system (Supervisory Control and Data Acquisition) is the software layer above it — the system that reads PLC tags, shows them on operator screens, logs them to a historian, and sends setpoint commands back down to the PLC. Most job postings that say "PLC SCADA" are asking for someone who can do both: write PLC logic that produces clean, well-named tags, and configure the SCADA system to read them correctly.
The PLC layer requires executable control logic; the SCADA layer adds its own engineering work in data modelling, alarm design, trends, security, redundancy and operator usability. This course begins with the PLC layer because every useful display value, alarm and command depends on a trustworthy controller tag underneath it.
Common question
PLC vs SCADA — and which to learn first
A PLC is the control layer: hardware that reads sensors and drives motors, valves, and lamps in real time. SCADA is the supervision layer: software that reads the PLC's tags, shows them on operator screens, logs them to a historian, raises alarms, and sends setpoints back down. SCADA cannot run without a PLC (or equivalent controller) producing the data underneath it.
That dependency answers the most common question — should I learn PLC or SCADA first? Learn the PLC data and control path first, then layer HMI, alarms, communications and historian concepts on top. SCADA is not merely drag-and-drop; starting with clean tags and predictable state makes the later engineering work testable instead of cosmetic.
Where does DCS fit? A Distributed Control System bundles the controller and supervisory layers into one vendor-integrated platform, used in continuous process plants (refining, chemicals, power). The tag, alarm, and loop-control concepts you build here transfer to DCS thinking too — the architecture differs, the control fundamentals do not.
How it fits together
The PLC + SCADA stack, illustrated
Each diagram below is a layer of the system this course teaches, from the field I/O up to the operator screen and the network that ties them together.
The supervisory layer — HMI/SCADA screens bound to live PLC tags.The controller — CPU, I/O modules, and the comms port SCADA reads from.Network topology — how PLCs and the SCADA server connect on the plant floor.Modbus TCP — coils and holding registers a SCADA driver reads from the PLC.Analog I/O scaling — raw counts to engineering units for the SCADA display.The scan cycle — the real-time loop SCADA samples its tag values from.Every SCADA tag starts as a PLC rung — the logic you write in this course.All in a browser tab — no Ignition or WinCC licence, no install.
Curriculum
PLC SCADA course curriculum
Six tracks from first principles to SCADA-ready. Estimated hours are for an engineer with no prior PLC experience working at a focused pace.
Track
What you learn
Est. hours
Certificate
Free?
PLC Fundamentals
Scan cycle, I/O addressing, contacts and coils, latching, timers, counters, state machines, debugging
8–16 hrs
Track progress recorded
Free
Core Building Blocks
Function blocks, structured text, analog I/O and scaling, sequence transitions and data movement
Machine logic plus 29 guided wiring labs and 19 guided fault-finding labs; access varies by plan
30–60 hrs
Scenario results recorded
Pro
HMI Track
Motor start/stop panel, alarm dashboard, multi-screen navigation, tag binding exercises
6–12 hrs
Practice evidence recorded
Pro
6 Interview Tracks
Timed scenario challenges: basic ladder, timers and counters, interlocks, sequencers
4–8 hrs
Eligible certificate on pass
Pro
Planning range: roughly 60–100+ focused hours for the controller-facing foundation, depending on prior electrical and programming experience. Production SCADA competence also requires vendor tools, supervised deployment and site experience.
Certification
What the completion evidence means
Eligible assessed Pro interview tracks can award a downloadable, publicly verifiable completion certificate after a passing result. The useful evidence is the work behind it: completed scenarios, repeated tests and an ability to explain the control path.
It is not a Rockwell, Siemens or ISA certification, an accredited qualification, a trade licence or authorization to work on live equipment. Use it as supporting portfolio evidence alongside supervised hardware practice and any credential required by your employer or jurisdiction.
Training cost and evidence vary by provider, region and delivery format. This comparison avoids temporary sale prices and shows the decision factors to verify before enrolling.
Option
Cost
Format
Hardware included
Certificate
Community college or technical institute
Check current local tuition and lab fees
Scheduled classroom or hybrid
Often, with instructor supervision
Provider-specific award
PLC or SCADA vendor training
Request current vendor or partner pricing
Classroom, virtual or e-learning
Depends on course format
Vendor or partner completion record
Video-first online marketplace course
Varies by provider and promotion
Self-paced video and quizzes
Usually not included
Platform completion badge
This platform — Pro
$29/month or $249/year
Broader browser practice and eligible assessed tracks
Simulation only
Eligible completion certificate on passing tracks
Verify current pricing, hardware access, refund terms, certificate status and prerequisites directly with each provider. This platform's prices above come from the versioned product facts used by the checkout and marketing surfaces.
Related
Related training pages
SCADA training — what SCADA roles need, skills matrix, and honest scope of what we teach.
PLC training — 55 learning modules and 170 source-catalogued practice records.
Eligible assessed Pro interview tracks can award a downloadable, publicly verifiable completion certificate after a passing result. It records work completed on this platform; it is not an accredited qualification, trade license, ISA credential or vendor certification.
A sound learning path covers the PLC scan and I/O model, ladder logic, tag architecture, HMI binding, alarms, analog scaling, industrial networking, Modbus data types, trends and PID setpoints. This platform teaches the controller-facing and HMI-practice foundation. Production historians, redundant SCADA servers, cybersecurity controls and vendor engineering tools require additional hands-on training.
Yes. Complete one guided first PLC program without an account. A free account includes 32 source-tagged catalog records and the first 6 core lessons in each learning dialect, with no card or trial expiry. HMI and SCADA-facing practice varies by plan and entitlement.
Classroom training can provide supervised hardware, instructor observation and a recognized local program. This browser course provides repeatable logic, HMI and diagnostic practice on a flexible schedule. The strongest path combines both: learn and rehearse online, then validate wiring, commissioning, safety and a production SCADA package under qualified supervision.
The exercises on this platform run in a modern browser, so you do not need a vendor IDE to start. That does not replace later experience in the actual engineering environment used at your plant, such as Studio 5000, TIA Portal, Ignition or WinCC.
Learn the PLC data and control path first, then the HMI and SCADA layer that observes and commands it. This order makes each display value, alarm and setpoint traceable to a real tag and physical purpose instead of treating SCADA as screen decoration.
Yes. Practice connects controller logic to observable machine I/O and HMI behavior. You can work through tags, interlocks, alarms and process states in repeatable simulations. Treat this as preparation for supervised commissioning, not as a substitute for testing the target controller, network, instruments and safety system.
It provides practical PLC and HMI foundations, including logic, tags, observable I/O and screen-to-tag behavior. Historian administration, reporting, redundancy, security hardening, proprietary drivers and production deployment still require a vendor SCADA package and supervised plant experience.
Competency and practice field guide
PLC and SCADA course: practice plan
Direct answer
The learner can prove one command and one measurement across field, PLC, communications and operator interface layers.
Written for learners connecting controller programs to HMI, alarm, trend and supervisory data workflows.
System map / 02
NODE 01observable
01
Scope
A control-and-supervision requirement with clear ownership.
NODE 02observable
02
Signal path
Field signals, PLC tags, protocol data and SCADA objects.
NODE 03observable
03
Baseline practice
Commands, feedback, alarms, trends and historian records.
NODE 04observable
04
Edge cases
Stale quality, command conflict, timeout and restart.
NODE 05observable
05
Fault practice
A field, logic, mapping or supervisory-layer fault.
NODE 06observable
06
Transfer to the job
The integrated case recreated in approved site tools.