TL;DR: An HMI (Human Machine Interface) is a touchscreen panel mounted at one machine that shows operators the live state of that machine's PLC. SCADA (Supervisory Control and Data Acquisition) is a server-based system that aggregates data from many PLCs and HMIs across an entire site or multiple sites, adds historical logging and alarm management, and gives remote visibility. An HMI is local and machine-specific. SCADA is site-wide and supervisory. A plant has one SCADA system, and dozens of HMI panels.
The confusion is understandable: both show process data on a screen, both have buttons operators can push, and modern SCADA software can render screens that look exactly like an HMI panel. But the scope, architecture, and purpose are fundamentally different — and knowing the distinction matters when you are specifying a project, troubleshooting a plant, or answering an interview question.
For the detailed breakdown of how HMI compares to PLC — who runs the logic, how tags work, what the HMI can and cannot do — see the dedicated PLC vs HMI post. This post focuses on the SCADA layer and why it exists above the HMI.
What an HMI Is
An HMI is a dedicated display device — typically a touchscreen panel — installed in or near the machine cabinet it serves. It communicates with one PLC (sometimes two, in redundant systems) over an Ethernet or fieldbus connection, reads PLC tag values, and displays them on configured screens. Operators use the HMI to start and stop equipment, change setpoints, acknowledge alarms, and view trends — but only for the machine that HMI is mounted at.
Key HMI characteristics:
- Panel-mounted or cabinet-mounted hardware at the machine.
- Communicates with one PLC; displays data from that PLC only.
- No historian: live data only, or short-term trend buffers (minutes to hours).
- Local alarm display: alarms from that machine only.
- If the HMI fails, the PLC keeps running. The operator loses the local screen but the machine continues.
Common HMI hardware: Siemens SIMATIC Basic/Comfort/Unified Panels, Allen-Bradley PanelView, Schneider Magelis, Weintek, Maple Systems.
What SCADA Is
SCADA is a software system running on a PC server that collects data from many PLCs and HMIs across a site using industrial protocols (OPC UA, EtherNet/IP, Modbus TCP, PROFINET). It stores that data in a historian database, displays it to operators on workstations anywhere on the plant network, manages alarm acknowledgement across the whole site, and generates reports.
Key SCADA characteristics:
- Server-based software, not a dedicated panel.
- Connects to many PLCs — tens to hundreds of devices.
- Historian: logs configured tags at defined intervals for months or years.
- Site-wide alarm management: one acknowledgement queue for every device on the network.
- If the SCADA server fails, every PLC and HMI panel keeps running locally. The operators lose the central view and remote control.
- Accessible from multiple operator workstations simultaneously.
Common SCADA platforms: Ignition (Inductive Automation), WinCC SCADA (Siemens), FactoryTalk View Site Edition (Rockwell), iFIX (GE/Proficy).
Side-by-Side Comparison
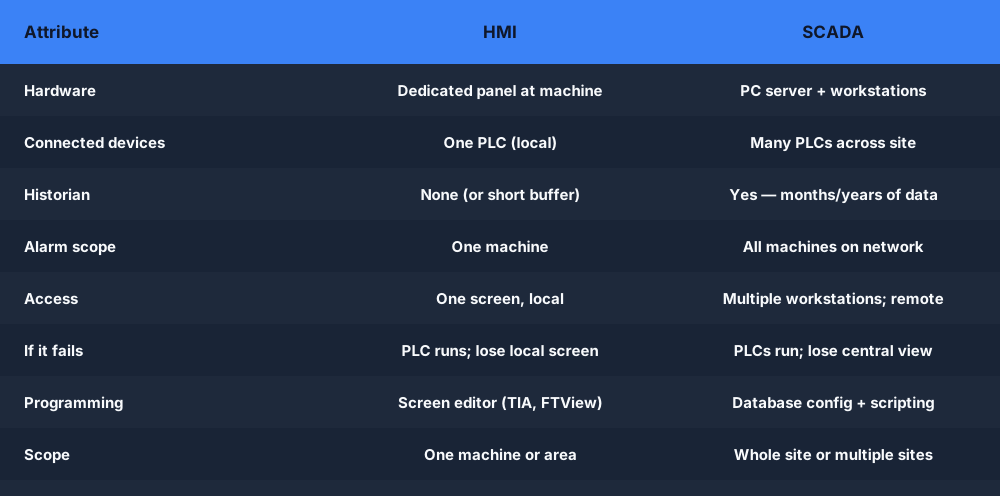
| HMI | SCADA | |
|---|---|---|
| Hardware | Dedicated panel at machine | PC server + workstations |
| Connected devices | One PLC (the local one) | Many PLCs across the site |
| Historian | None (or short buffer) | Yes — months or years of data |
| Alarm scope | One machine's alarms | All machines on the network |
| Access | One screen, physically local | Multiple workstations; remote access |
| Trend data | Short buffer only | Long-term trending, report generation |
| If it fails | PLC keeps running; lose local screen | PLCs keep running; lose central view |
| Programming | Screen editor (TIA, FactoryTalk, etc.) | Database config + scripting |
| Scope | One machine or area | Whole site or multiple sites |
The Architecture Stack
It helps to think in layers. From physical hardware to site-wide oversight:
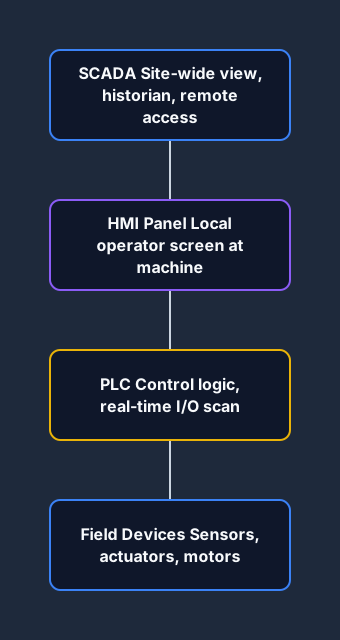
Layer 1: Field devices. Sensors, actuators, motors — physical hardware.
Layer 2: PLC. Reads sensors, runs logic, drives actuators. Deterministic, real-time. One per machine or process unit.
Layer 3: HMI. The operator panel at the machine. Reads and writes to the local PLC. Local visibility only.
Layer 4: SCADA. Reads from many PLCs across the plant network. Historian, alarms, reporting, remote access. Site-wide visibility.
SCADA does not replace the HMI. In most large sites, both exist. The machine operator uses the local HMI panel; the shift supervisor and plant manager use the SCADA workstation. The process engineer pulls historian trends from SCADA for analysis. Both layers serve different audiences.
When You Only Need an HMI
Not every site needs SCADA. A single machine — a packing machine, an injection moulding press, a water pump skid — is completely served by a PLC and an HMI panel. There is no need for site-wide historian or centralized alarm management when there is only one machine to watch.
Small manufacturing facilities, standalone machines in workshops, and process units that are maintained independently all fit this pattern. PLC + HMI is the standard configuration for most industrial machines sold as units.
When You Need SCADA on Top
SCADA becomes necessary when:
- You have multiple machines or process units to watch simultaneously.
- You need historical trending to investigate process problems (why did the pressure spike at 2:14 AM last Tuesday?).
- You need to generate reports — production totals, OEE, alarm statistics, regulatory compliance data.
- You need remote access — operators monitoring from a control room, managers viewing KPIs from an office, remote access for engineers troubleshooting from outside the plant.
- You have geographically distributed assets — pump stations, pipeline valves, remote generator sets.
Real Plant Example
A bottling plant has eight filling lines, each with a Siemens S7-1500 PLC and a 15-inch SIMATIC Comfort Panel HMI. The operator on each line uses the local HMI to start fills, adjust fill volume setpoints, and acknowledge local alarms.
In the plant manager's office, an Ignition SCADA server displays a dashboard showing all eight lines simultaneously: current fill rate, bottle count, downtime status, and active alarms. The production engineer uses Ignition's historian to pull trend data for quality review. The maintenance manager has a remote access client on his phone.
The local HMI panels would function identically with or without the Ignition server running. Ignition adds the plant-wide layer; the HMIs serve the machine layer.
Common Confusions Cleared Up
"The HMI is a dumb terminal for SCADA." An HMI is an independent device communicating directly with its local PLC. It does not depend on the SCADA server to function. In sites where both exist, the HMI gets its data from the PLC, and SCADA independently also polls the PLC. They read the same source independently.
"Modern HMI software can do everything SCADA does." Some modern HMI platforms (Siemens WinCC Unified, Allen-Bradley Studio 5000 View Designer) have added historian and alarm management capabilities. The boundary is blurring. But a traditional PanelView or SIMATIC Basic Panel is purely local — it has no historian and serves only its local PLC.
"SCADA is just a web version of the HMI." Web-based SCADA rendering (Ignition's web client, for example) means you can access a SCADA view from a browser. But the SCADA server behind it is collecting from dozens of PLCs, maintaining a historian, and managing site-wide alarms. The web rendering is just the display layer.
Frequently Asked Questions
Q: Do I need SCADA if I have an HMI?
A: Not necessarily. A single machine with a PLC and HMI is completely functional without SCADA. SCADA adds value when you need to watch multiple machines, log historical data long-term, or access the system remotely. If the question is whether you need both: it depends entirely on the scale of your site and what visibility you need.
Q: Can SCADA replace the HMI panel?
A: In theory, a SCADA screen on a workstation can serve as the operator interface for a machine, removing the need for a dedicated HMI panel. Some sites do this — thin-client workstations at machines, all displaying SCADA screens. The tradeoff is that machine-level visibility is now dependent on the SCADA server being reachable. In practice, panel-mounted HMIs remain standard for machine-level control because of their reliability and independence.
Q: What is the difference between SCADA and a historian?
A: The historian is one component inside a SCADA system — the database that stores time-series process values. SCADA is the full platform: historian + display + alarming + reporting + remote access. Some plants buy a standalone historian (OSIsoft PI, AVEVA Historian) separately from their SCADA platform and integrate them.
Q: Which should I learn first, HMI or SCADA?
A: HMI first. HMI programming teaches you tags, screen building, alarm configuration, and PLC communication — all of which are the same concepts in SCADA, just at larger scale. The HMI programming tutorial covers the basics. Once you understand how an HMI connects to a PLC, how tags bind to display objects, and how alarms work, SCADA is a natural progression.
The PLC logic that feeds both HMI panels and SCADA is where it starts. Practice the ladder logic side in the free browser simulator — no installation, no hardware required.
