Basic
20 min

Case Packer

packagingcounterpusherconveyor

Ready to build this?

Sign up free — no credit card required. This scenario requires the Basic plan.

Sign up to play this scenario →

Already have an account? Log in

Case Packer scenario preview

Briefing

A case packer accumulates products from a conveyor until the target count (12 per case) is reached, then a pusher loads them into an open case. Once the PACKING_COMPLETE_LS confirms the case is full, CASE_SEAL pulses to seal the case, the count resets, and the machine waits for the next case.

Objectives

  • COUNT_SENSOR increments the product counter on each rising edge (while running)
  • When count reaches 12 (target), DIVERTER activates to stop new products entering
  • PUSHER activates when count is at target AND CASE_READY
  • PACKING_COMPLETE_LS triggers CASE_SEAL pulse (500ms), then count resets
  • READY_LAMP on while count < target and CASE_READY (ready to accept product)
  • STOP_PB resets count and de-energises all outputs

Hints

  • Use a rising-edge detect on COUNT_SENSOR to increment CTU
  • COUNT_SENSOR.CV >= 12 sets DIVERTER and enables pusher
  • CASE_SEAL is a TON-timed pulse (500ms) triggered by PACKING_COMPLETE_LS
  • Reset CTU when CASE_SEAL finishes (new case)

I/O Table

Inputs

PRODUCT_DETECTED

Product presence sensor

BOOL · %I0.0

COUNT_SENSOR

Product count pulse sensor

BOOL · %I0.1

CASE_READY

Empty case in position

BOOL · %I0.2

PACKING_COMPLETE_LS

Limit switch — pusher at full stroke

BOOL · %I0.3

START_PB

Start push-button

BOOL · %I0.4

STOP_PB

Stop push-button

BOOL · %I0.5

Outputs

DIVERTER

Product diverter (stops new product)

BOOL · %Q0.0

PUSHER

Product pusher into case

BOOL · %Q0.1

CASE_SEAL

Case sealer (500ms pulse)

BOOL · %Q0.2

READY_LAMP

Ready to accept products indicator lamp

BOOL · %Q0.3

Your program will be tested against:

All test cases run automatically when you submit. Assertions are hidden until you pass.

  1. #1READY_LAMP on when running and case ready

    START_PB + CASE_READY -> READY_LAMP

  2. #2COUNT_SENSOR pulses increment product count

    Physics counts product pulses and pushes count state

  3. #3DIVERTER activates when count reaches target

    12 count pulses -> DIVERTER on

  4. #4PACKING_COMPLETE_LS triggers case seal and count reset

    After pushing, LS triggers seal, count resets

Ready to build this?

Sign up free — no credit card required. This scenario requires the Basic plan.

Sign up to play this scenario →

Already have an account? Log in

Runnable simulator field guide

Case-packer PLC scenario: test checklist

Direct answer

The learner can build one state-owned pack cycle, maintain count-to-case association, block conflicting motion and recover from a known material state.

Written for packaging automation learners coordinating product infeed, carton presence, grouped transfer, flap or discharge actions and fault recovery.
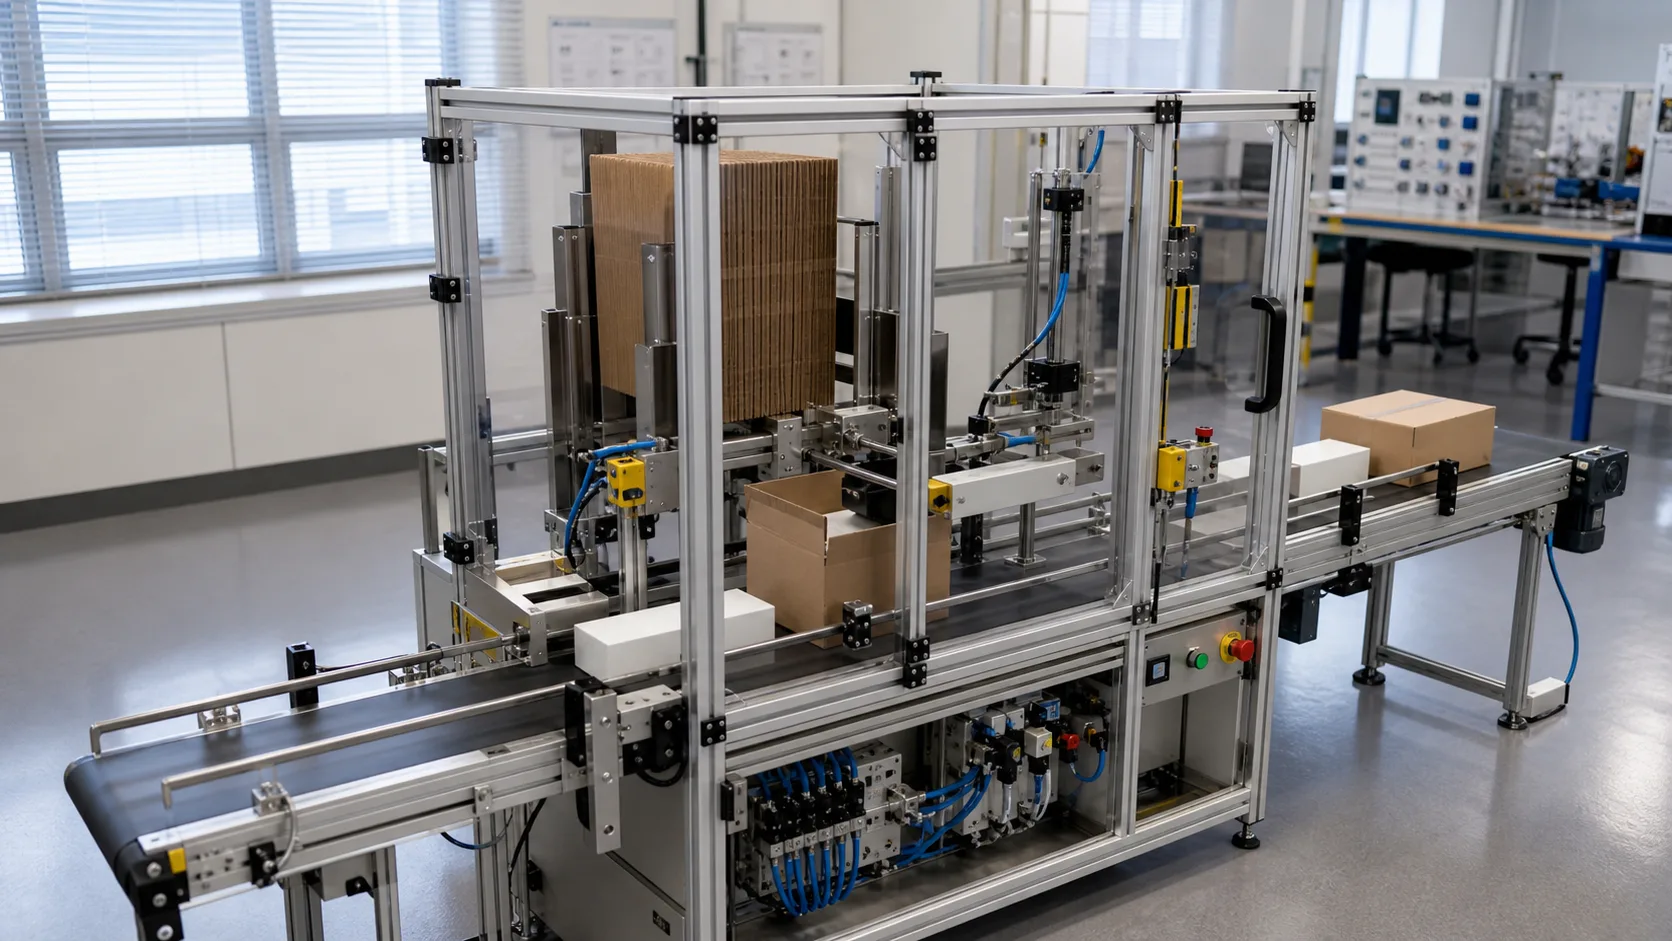
a guarded case-packing training cell with cartons, conveyors, sensors and a pneumatic transfer mechanism while studying case-packer product counting, carton readiness, transfer sequencing and jam recovery
System map / 02

NODE 01observable

Scenario setup

Product detection, count edge, target pack quantity, carton available and positioned, pusher home and extend proof, discharge clear, state owner, timeout and reject or recovery policy.

NODE 02observable

I/O and state map

Products through sensing and count state to full-group decision, carton permissive, transfer command, motion feedback, packed-case confirmation and discharge.

NODE 03observable

Normal run

One declared group enters one ready case, transfer proves both positions, count resets once and the packed case clears before the next cycle.

NODE 04observable

Boundary run

Missing carton, double product, sensor bounce, count mismatch, pusher timeout, carton shift, blocked discharge, stop, restart and partial group.

NODE 05observable

Injected fault

A product, sensor, count, carton, state, command, actuator, feedback, timing or recovery mismatch.

NODE 06observable

Target check

The sequence recreated with exact mechanics, guarding, motion, product and carton acceptance tests.

Answer surface / 07

How should a PLC track products into a case packer?

Create one event per accepted product, associate the count with a declared group and reset only after transfer and packed-case confirmation, not merely after issuing a pusher command.

What should happen after a stop with a partial product group?

The recovery policy must use actual product, carton and mechanism state; either resume the identified group or clear it through a controlled manual procedure.