Runnable simulator field guide
Simple palletizer PLC scenario: test checklist
Direct answer
The learner can define explicit states, prove every material movement with sensors, prevent duplicate counts and recover from a stopped or missing-item condition.
Written for pLC learners programming a guarded compact palletizing model with conveyor sensing, part counts, transfer motion and layer completion.
Scenario setup
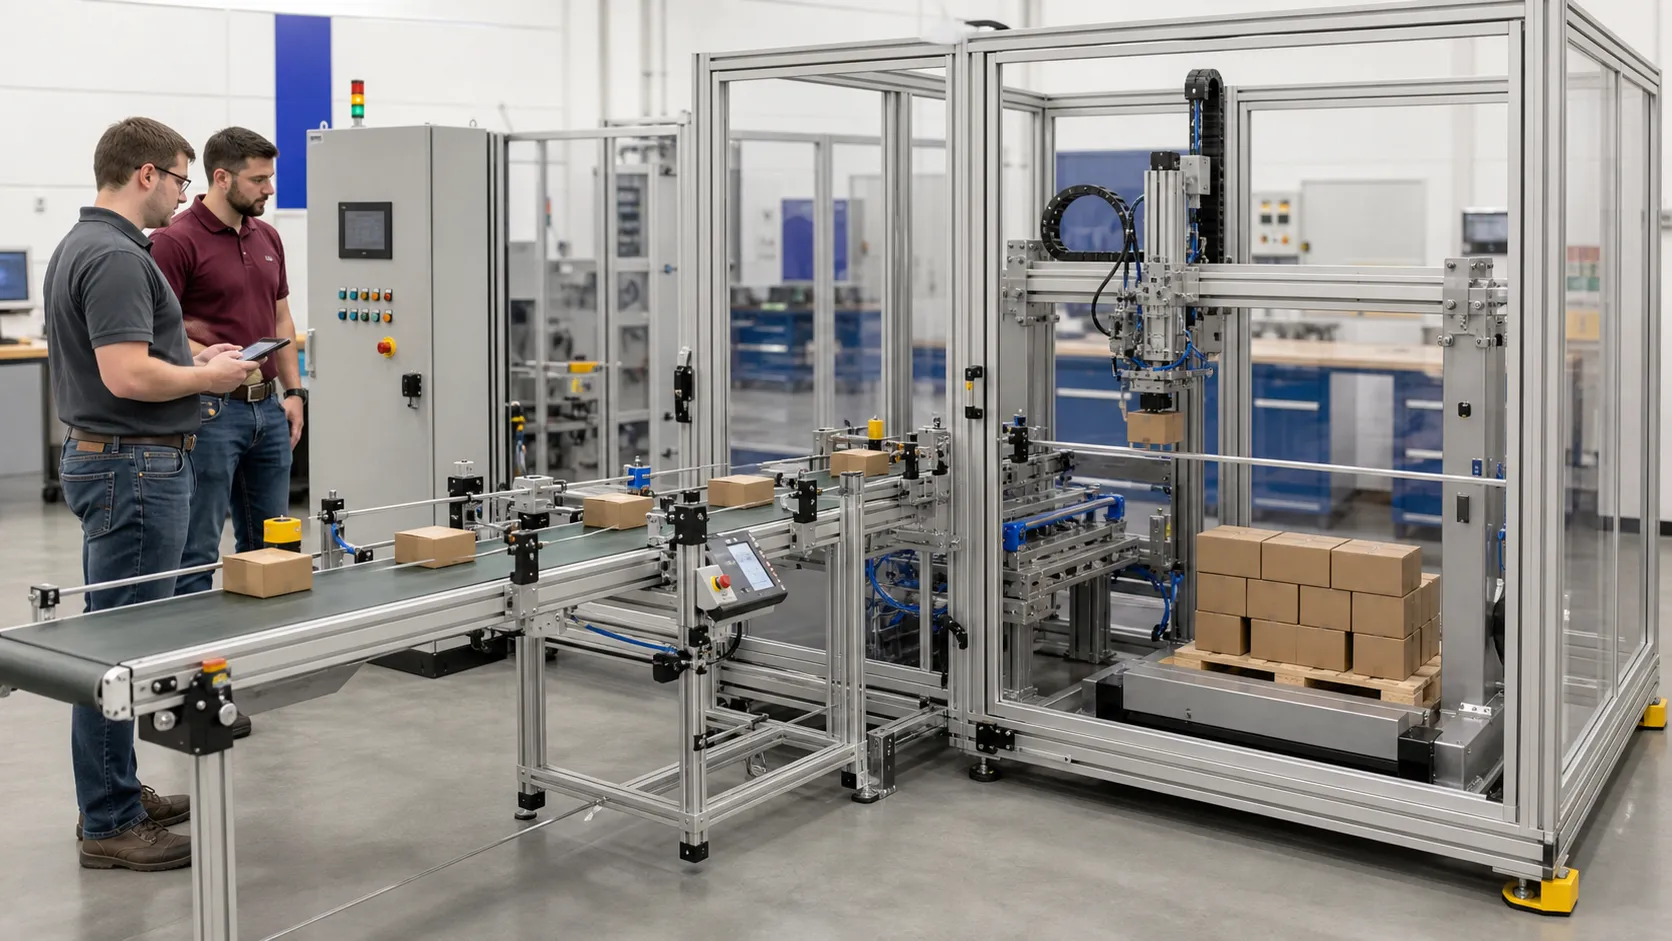
Product and pallet model, infeed sensor, accumulation, part count, row and layer pattern, transfer axes or pneumatic motion, end feedback, interlocks, timeout, stop and restart policy.
I/O and state map
Product arrival through detection and count to accumulation, transfer command, position proof, pallet placement, pattern update, completed layer and release.
Normal run
Representative products are counted once and placed in the declared pattern with every motion and completion transition proved.
Boundary run
Held photoeye, missing carton, double product, count mismatch, axis timeout, full pallet, pallet absent, interruption, reset and power return.
Injected fault
A material, sensor, count, pattern, state, command, axis, feedback, timeout or restart mismatch.
Target check
The control behavior transferred into a guarded target cell with motion, payload, safety and throughput validation.
What logic does a simple palletizer need?
It needs material detection, one-event counting, accumulation, explicit transfer states, position feedback, pallet presence, pattern tracking, timeouts and controlled recovery.
Why should palletizer count and motion state be separate?
A count records material history while motion state controls current action; combining them makes missing or repeated transfers harder to diagnose.