Basic
20 min

3-Way Sortation Diverter

conveyorsortationdiverteritem-trackingfault

Ready to build this?

Sign up free — no credit card required. This scenario requires the Basic plan.

Sign up to play this scenario →

Already have an account? Log in

3-Way Sortation Diverter scenario preview

Briefing

An extension of the 2-way sortation diverter with a third lane. Each item passes a photoeye and carries exactly one tag (TAG_A, TAG_B, or TAG_C). After a 500 ms travel delay the correct diverter solenoid energises for 1 s to route the item into the corresponding lane. Multi-tag reads (more than one tag high) or zero-tag reads latch ERROR_LAMP. STOP_PB clears the error and halts the conveyor.

Objectives

  • CONV_RUN is on whenever the system is running (not stopped)
  • On PHOTOEYE_IN rising edge, latch tag values; validate exactly one tag set
  • After 500 ms travel delay, energise the correct diverter (A, B, or C) for 1 s
  • Multi-tag or zero-tag reads latch ERROR_LAMP and suppress diverter action
  • ERROR_LAMP latches until STOP_PB is pressed with all tags de-asserted

Hints

  • Capture tags on PHOTOEYE_IN one-shot: ITEM_A := TAG_A; ITEM_B := TAG_B; ITEM_C := TAG_C
  • Validate: VALID := (ITEM_A XOR ITEM_B XOR ITEM_C) AND NOT (ITEM_A AND ITEM_B) AND NOT (ITEM_A AND ITEM_C) AND NOT (ITEM_B AND ITEM_C)
  • Use TON_TRAVEL (500 ms) then TON_DIVERT (1 s) after valid detection
  • ERROR_BIT: S= on invalid tag, R= on STOP_PB AND NOT TAG_A AND NOT TAG_B AND NOT TAG_C

I/O Table

Inputs

PHOTOEYE_IN

Photoeye — item at entry zone

BOOL · %I0.0

TAG_A

Tag read: item is Type A

BOOL · %I0.1

TAG_B

Tag read: item is Type B

BOOL · %I0.2

TAG_C

Tag read: item is Type C

BOOL · %I0.3

DIVERTER_A_HOME

Diverter A at home position

BOOL · %I0.4

DIVERTER_B_HOME

Diverter B at home position

BOOL · %I0.5

DIVERTER_C_HOME

Diverter C at home position

BOOL · %I0.6

STOP_PB

Stop / fault-reset push-button

BOOL · %I0.7

Outputs

CONV_RUN

Conveyor drive run

BOOL · %Q0.0

DIVERTER_A

Diverter A solenoid

BOOL · %Q0.1

DIVERTER_B

Diverter B solenoid

BOOL · %Q0.2

DIVERTER_C

Diverter C solenoid

BOOL · %Q0.3

ERROR_LAMP

Error indicator lamp (latching)

BOOL · %Q0.4

Your program will be tested against:

All test cases run automatically when you submit. Assertions are hidden until you pass.

  1. #1CONV_RUN on by default, stops on STOP_PB

    Conveyor runs immediately; STOP_PB drops it

  2. #2TAG_A item activates DIVERTER_A after 500ms

    Single TAG_A read routes item to lane A

  3. #3TAG_C item activates DIVERTER_C

    Single TAG_C read routes item to lane C

  4. #4TAG_B item activates DIVERTER_B after 500ms

    Single TAG_B read routes the item to lane B without energising either neighbouring diverter

  5. #5Multi-tag read latches ERROR_LAMP

    TAG_A and TAG_B both set causes error; STOP_PB clears

  6. #6Zero-tag read latches ERROR_LAMP

    No tag asserted when photoeye fires causes error

Ready to build this?

Sign up free — no credit card required. This scenario requires the Basic plan.

Sign up to play this scenario →

Already have an account? Log in

Runnable simulator field guide

Three-way sortation diverter scenario: test checklist

Direct answer

The learner can associate one accepted product with one route decision, actuate at the correct position and confirm the actual destination before releasing tracking state.

Written for pLC programmers building deterministic routing for products that must reach one of three conveyor destinations.
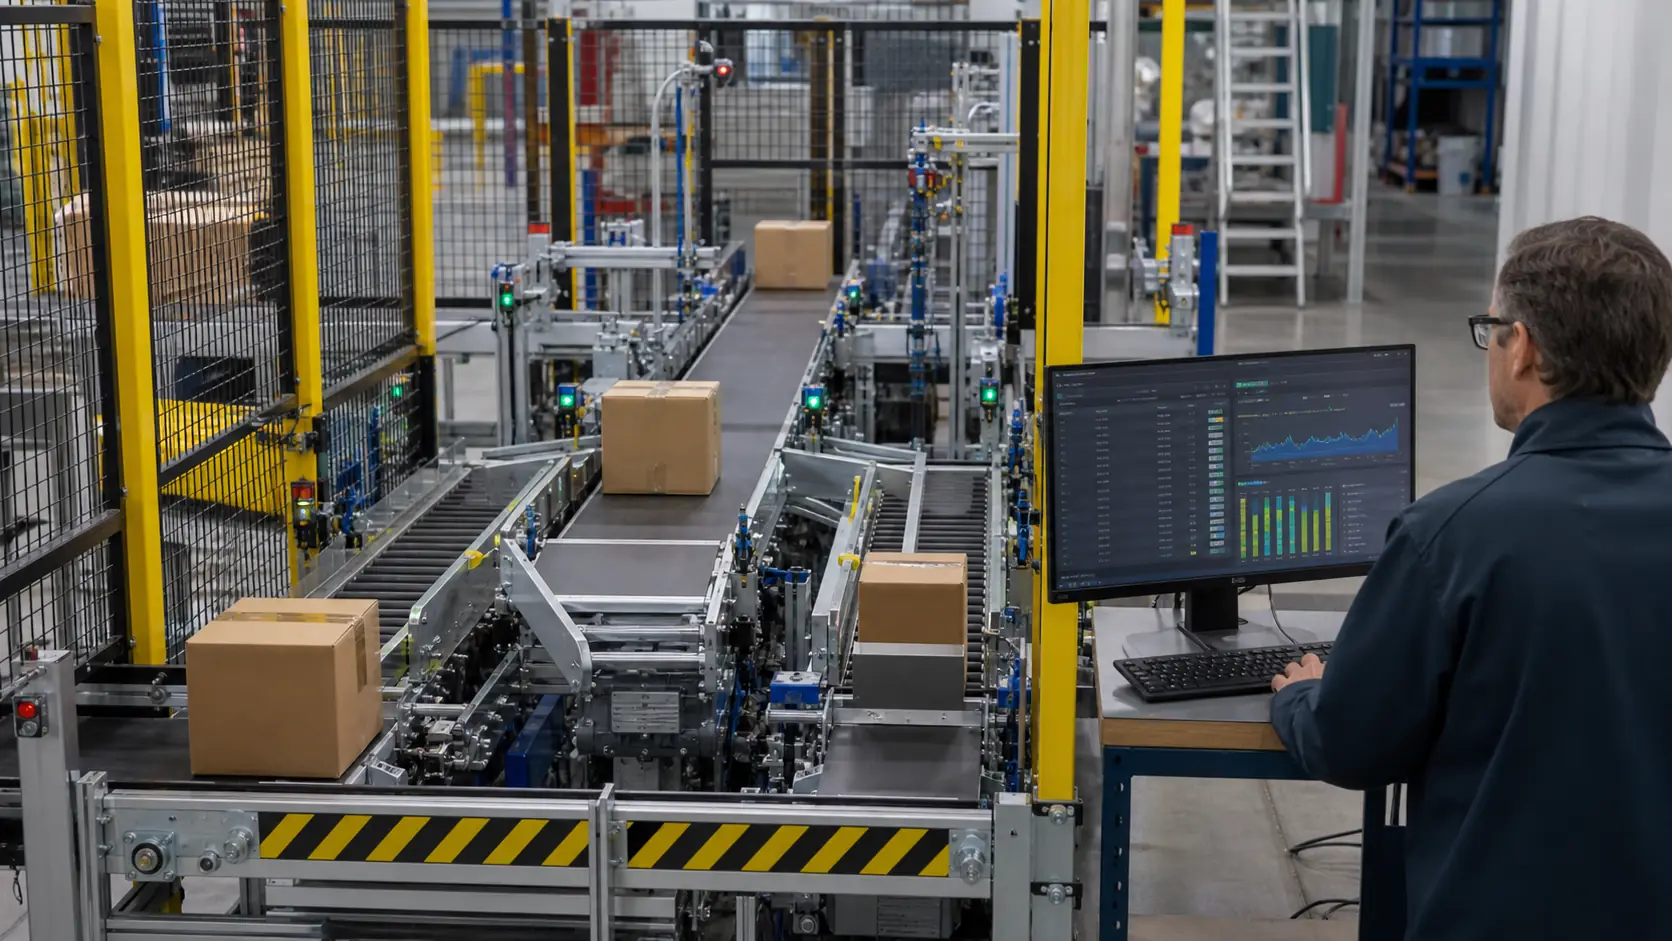
a guarded conveyor sortation cell with three destinations, photoelectric sensing, pneumatic diversion and package confirmation while studying three-destination routing, package tracking, actuator confirmation and jam recovery
System map / 02

NODE 01observable

Scenario setup

Product identity, classification, entry event, travel model, route decision, diverter position, actuation window, destination confirmation and reject policy.

NODE 02observable

I/O and state map

Accepted product through tracking state and position into route arbitration, actuator command, physical gate response and destination sensor.

NODE 03observable

Normal run

One product at a time reaching each of three destinations with exactly one decision, one command window and one confirmation.

NODE 04observable

Boundary run

Closely spaced products, missing classification, conflicting route, late actuator, sensor bounce, jam, stop mid-transfer, restart and manual clear.

NODE 05observable

Injected fault

An identity, classification, tracking, position, arbitration, output, actuator, destination or recovery mismatch.

NODE 06observable

Target check

The sequence replayed with recorded timing margins and then commissioned against real conveyor dynamics, guarding and device feedback.

Answer surface / 07

How does a PLC control a three-way diverter?

It retains each product’s destination, tracks the product to the diversion point, arbitrates one route, commands the mechanism inside a valid window and confirms the actual destination.

How should a sorter recover after a jam?

Freeze or reconcile tracking against actual product positions, remove the cause under the approved procedure, establish a known state and test the affected route before automatic release.