Pro
15 min

Lesson 11 — Conveyor Reject

curriculumlessonmixedconveyorcounter

Ready to build this?

Sign up free — no credit card required. This scenario requires the Pro plan.

Sign up to play this scenario →

Already have an account? Log in

Lesson 11 — Conveyor Reject scenario preview

Briefing

Bring it all together: a conveyor with a photoelectric sensor, a counter, and a reject gate. Parts pass the PHOTO_EYE sensor. Every 5th part is rejected by the REJECT_GATE. The CONV_RUN motor runs while ENABLE is true. This lesson combines Lessons 1-10.

Objectives

  • CONV_RUN follows ENABLE (seal-in not required here)
  • Each PHOTO_EYE rising edge increments the count
  • REJECT_GATE activates on every 5th part (when CTU.CV mod 5 === 0)

Hints

  • Run the conveyor: | ENABLE | := CONV_RUN ;
  • Count parts with CTU(CU := PHOTO_EYE, R := REJECT_GATE, PV := 5);

I/O Table

Inputs

ENABLE

Conveyor enable

BOOL · %I0.0

PHOTO_EYE

Part detected sensor

BOOL · %I0.1

Outputs

CONV_RUN

Conveyor motor run

BOOL · %Q0.0

REJECT_GATE

Reject gate solenoid

BOOL · %Q0.1

Your program will be tested against:

All test cases run automatically when you submit. Assertions are hidden until you pass.

  1. #1CONV_RUN follows ENABLE

    Conveyor must run when enable is on

  2. #25th part triggers REJECT_GATE

    5 photoelectric pulses should activate the reject gate

Ready to build this?

Sign up free — no credit card required. This scenario requires the Pro plan.

Sign up to play this scenario →

Already have an account? Log in

Competency and practice field guide

Mixed PLC instructions curriculum scenario: practice plan

Direct answer

The learner can assign clear state ownership, predict scan-order interactions and prove normal, simultaneous, fault and restart cases.

Written for pLC learners integrating individually understood instructions into a complete, testable machine behavior.
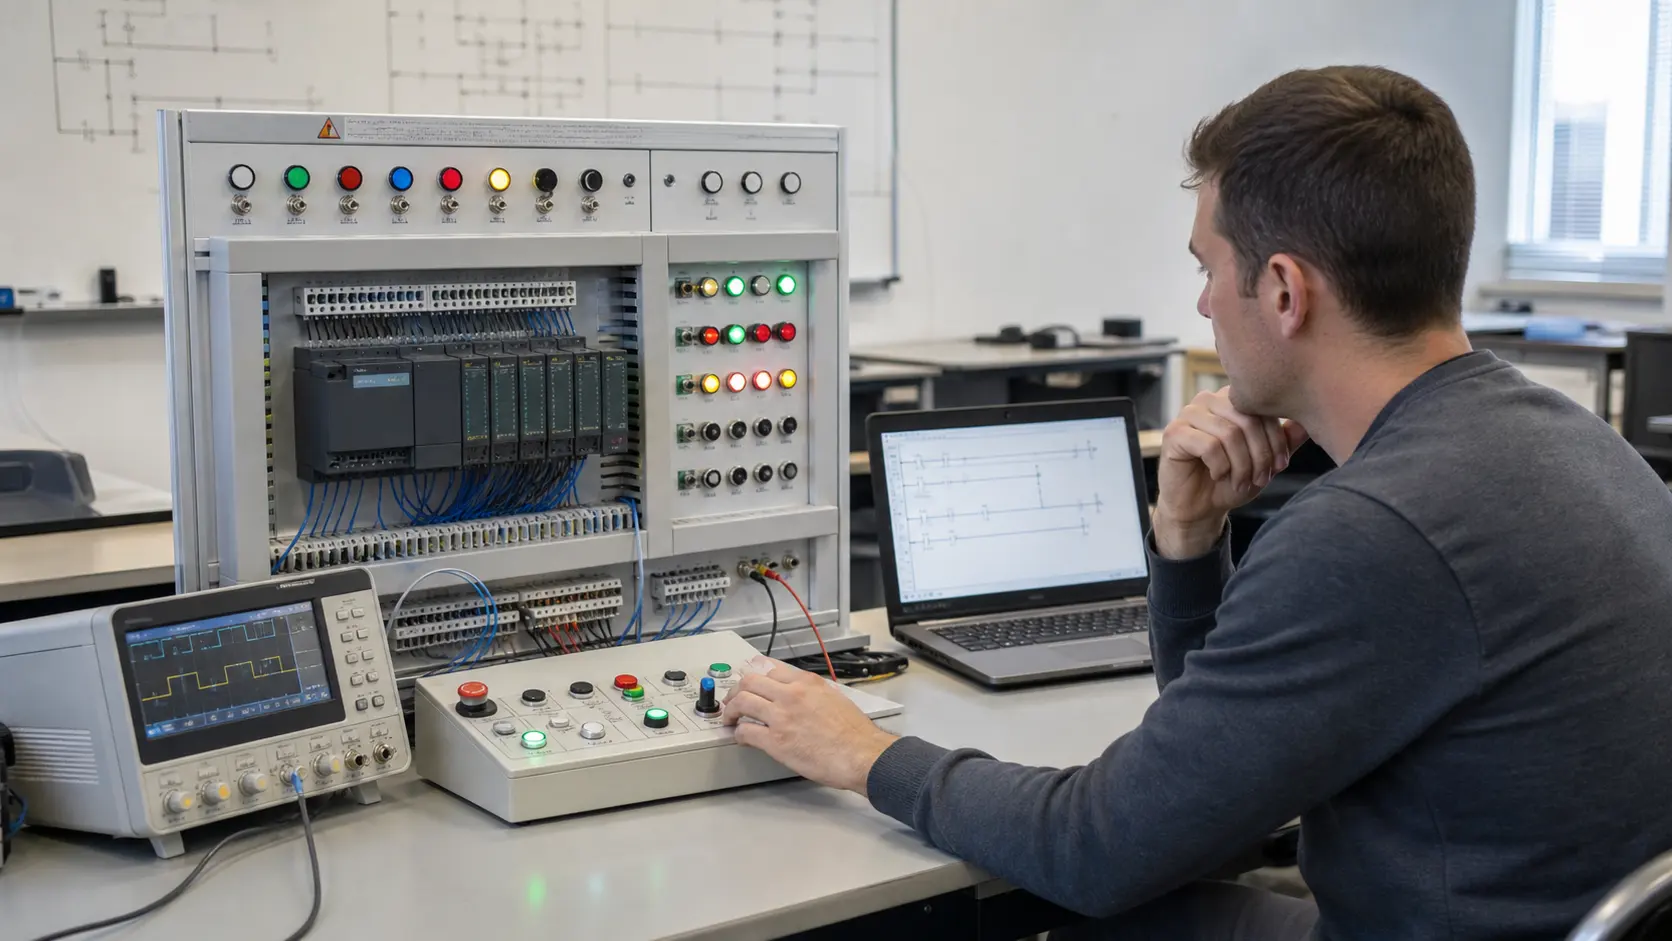
a PLC logic and scan-cycle training station with observable inputs, outputs, timing traces and program state used to prove execution behavior while studying combined Boolean, edge, timer, counter and state behavior in one PLC sequence
System map / 02

NODE 01observable

Scope

Input truth, stop priority, internal state, edge memory, timer and counter state, comparison, output ownership, feedback and restart policy.

NODE 02observable

Signal path

Sampled inputs through ordered rung or statement execution to state transitions, final outputs, machine response and feedback.

NODE 03observable

Baseline practice

A declared multi-step cycle starts, advances, counts, times and stops repeatedly from one clean initial state.

NODE 04observable

Edge cases

Simultaneous start and stop, held sensor, extra edge, timer equality, counter rollover, fault during state, power return and manual reset.

NODE 05observable

Fault practice

An input, instruction-state, scan-order, state-owner, timer, counter, output, feedback or restart mismatch.

NODE 06observable

Transfer to the job

The behavior recreated in official tools with exact data types, scheduling and target I/O checks.

Answer surface / 07

How do you combine timers and counters safely in PLC logic?

Give each function a clear enable and reset contract, use explicit state ownership and test scan-order and restart cases instead of chaining status bits by intuition.

Why does mixed PLC logic pass simple tests but fail in a sequence?

Interactions between retained state, edges, timing, output ownership and simultaneous events appear only when the complete scan and machine state are exercised.