Basic
40 min

CIP Sequence Controller

sequencefood-beverageciptimersprocess

Ready to build this?

Sign up free — no credit card required. This scenario requires the Basic plan.

Sign up to play this scenario →

Already have an account? Log in

CIP Sequence Controller scenario preview

Briefing

Clean-in-Place (CIP) is a fully automated cleaning sequence used in food and beverage processing. Your controller must step a vessel through five cleaning stages — Pre-Rinse, Caustic wash, Intermediate Rinse, Acid wash, and Final Rinse — each timed precisely. The pump and heater must be managed correctly per stage, and the FLOW_OK and TEMP_OK process interlocks must be satisfied before the cycle is considered healthy. Pressing STOP_PB at any time aborts the sequence and returns to IDLE.

Objectives

  • START_PB begins the sequence from IDLE
  • PRE_RINSE (3 s): open VALVE_RINSE + run PUMP_RUN
  • CAUSTIC (6 s): open VALVE_CAUSTIC + run PUMP_RUN + HEATER_ON
  • INTERMEDIATE_RINSE (3 s): open VALVE_RINSE + run PUMP_RUN
  • ACID (4.5 s): open VALVE_ACID + run PUMP_RUN + HEATER_ON
  • FINAL_RINSE (3 s): open VALVE_RINSE + run PUMP_RUN, then assert CYCLE_COMPLETE_LAMP
  • STOP_PB aborts the sequence at any stage and closes all outputs
  • FAULT_LAMP asserts if pump stops unexpectedly during an active stage

Hints

  • Use a step counter (INT) or a chain of latching bits: STEP_PRE_RINSE, STEP_CAUSTIC …
  • Use TON timers — one per step, chained so the Q output advances to the next step
  • VALVE_RINSE := STEP_PRE_RINSE OR STEP_INTERMEDIATE_RINSE OR STEP_FINAL_RINSE
  • HEATER_ON := STEP_CAUSTIC OR STEP_ACID; only these steps need TEMP_OK satisfied
  • CYCLE_COMPLETE_LAMP latches SET at the end of FINAL_RINSE; R= on START_PB

I/O Table

Inputs

START_PB

Start push-button

BOOL · %I0.0

STOP_PB

Stop / abort push-button

BOOL · %I0.1

FLOW_OK

Flow switch (asserts ~0.5 s after pump+valve)

BOOL · %I0.2

TEMP_OK

Temperature at setpoint (asserts ~1 s after heater on)

BOOL · %I0.3

Outputs

VALVE_RINSE

Rinse water supply valve

BOOL · %Q0.0

VALVE_CAUSTIC

Caustic solution valve

BOOL · %Q0.1

VALVE_ACID

Acid solution valve

BOOL · %Q0.2

PUMP_RUN

Circulation pump

BOOL · %Q0.3

HEATER_ON

Tank heater (caustic + acid stages)

BOOL · %Q0.4

CYCLE_COMPLETE_LAMP

Cycle complete indicator lamp

BOOL · %Q0.5

FAULT_LAMP

Fault indicator lamp

BOOL · %Q0.6

Your program will be tested against:

All test cases run automatically when you submit. Assertions are hidden until you pass.

  1. #1START_PB opens VALVE_RINSE and runs pump (PRE_RINSE)

    Press START_PB; VALVE_RINSE and PUMP_RUN must assert; no caustic or acid valve

  2. #2CAUSTIC step opens VALVE_CAUSTIC + HEATER_ON

    After PRE_RINSE completes, VALVE_CAUSTIC and HEATER_ON must be on

  3. #3Lost flow during an active wash latches FAULT_LAMP

    Start pre-rinse, then force FLOW_OK false after it had settled; the fault indicator must latch

  4. #4CYCLE_COMPLETE_LAMP asserts after all steps finish

    Run the full sequence; CYCLE_COMPLETE_LAMP should assert at end

  5. #5STOP_PB aborts mid-sequence and closes all outputs

    Start the sequence, press STOP during PRE_RINSE; all outputs must go off

  6. #6ACID step opens VALVE_ACID and runs heater

    After pre-rinse + caustic + intermediate rinse, VALVE_ACID and HEATER_ON must be on

Ready to build this?

Sign up free — no credit card required. This scenario requires the Basic plan.

Sign up to play this scenario →

Already have an account? Log in

Runnable simulator field guide

Clean-in-place PLC sequence scenario: test checklist

Direct answer

The learner can define every phase transition, prove valve and pump paths, handle missing temperature, flow or conductivity evidence and return safely from a held sequence.

Written for process-control learners implementing pre-rinse, chemical circulation, intermediate rinse and final rinse states with verified routes and conditions.
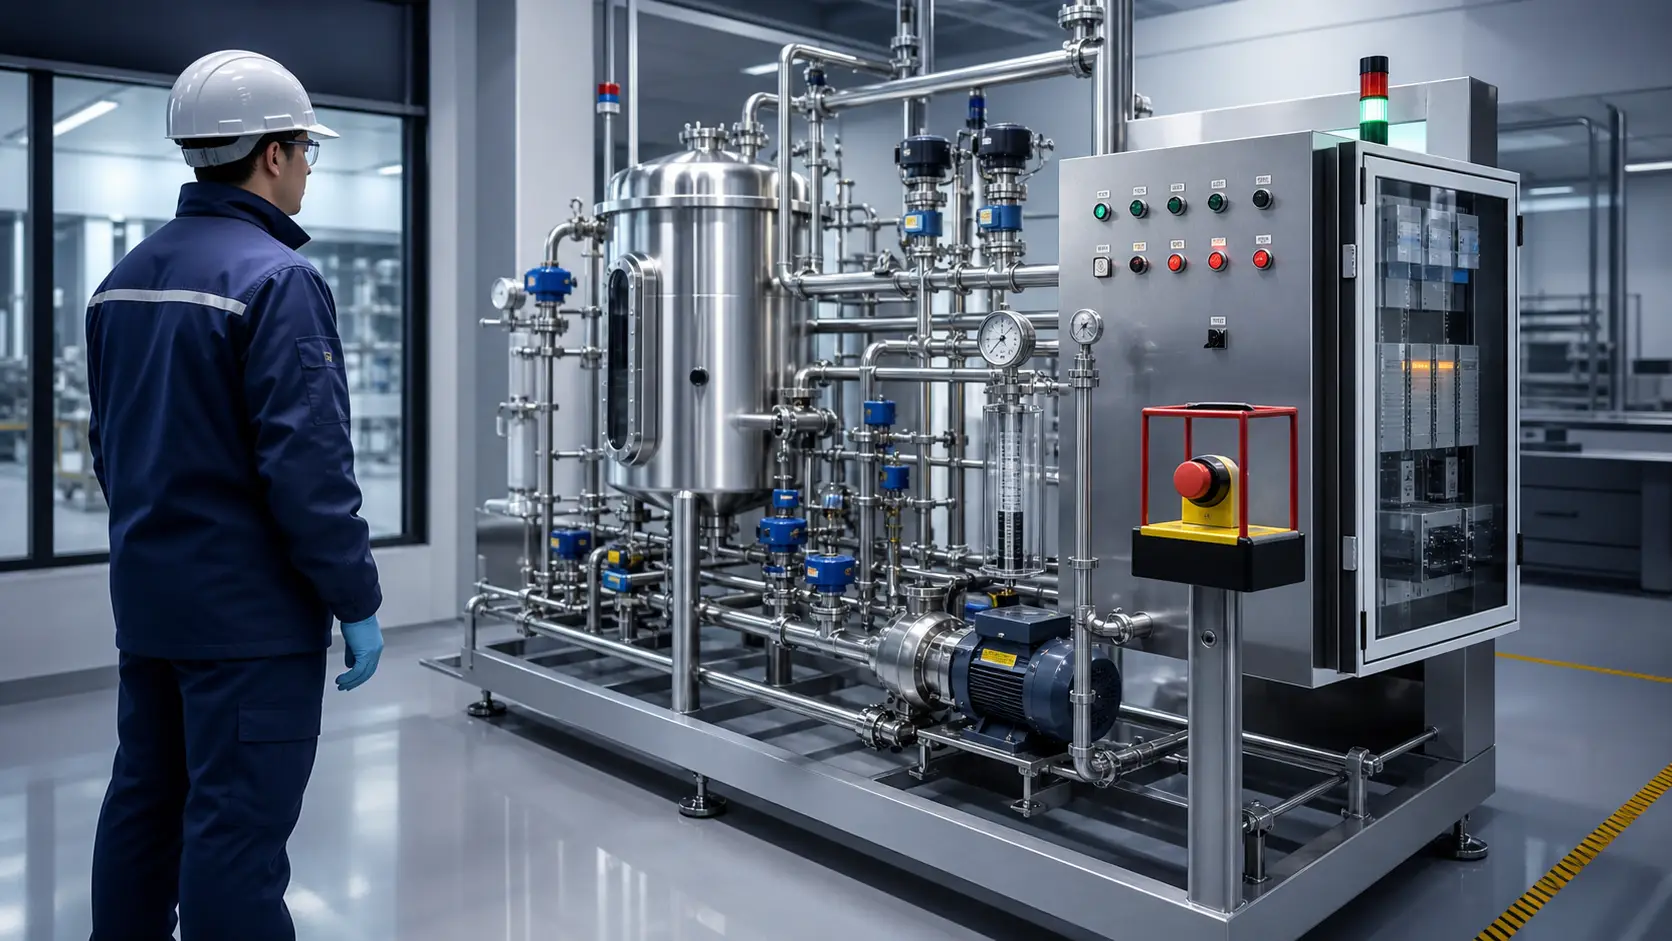
a guarded stainless process training skid used to validate clean-in-place and emergency-shutdown sequence states, instruments and feedback while studying CIP phase sequencing, permissives, proof, hold and recovery
System map / 02

NODE 01observable

Scenario setup

Equipment boundary, recipe phases, route selection, valve matrix, pump permissives, flow, temperature, concentration or conductivity, time, drain state and hold policy.

NODE 02observable

I/O and state map

Operator request through route confirmation, phase state, valve commands, pump command, process proofs, completion criteria, record and next phase.

NODE 03observable

Normal run

Each phase starts only with the declared route and proofs, meets its completion criteria and transitions once.

NODE 04observable

Boundary run

Empty supply, wrong route, failed valve feedback, no flow, low temperature, concentration drift, pause, abort, restart and recovery.

NODE 05observable

Injected fault

A recipe, state, route, valve, pump, instrument, timer, completion, hold or record mismatch.

NODE 06observable

Target check

The sequence reviewed against current process, equipment, chemical, safety and quality requirements and witnessed on target.

Answer surface / 07

What is a CIP sequence?

It is a controlled progression of cleaning phases with defined routes, media, flow, temperature, concentration, timing, proof and records.

Why should CIP transitions use proof instead of time alone?

Time cannot confirm the intended route, flow, temperature or chemistry; phase completion should use the evidence required by the validated process.